
In the pursuit of advancing renewable energy technologies, thin film solar panels have emerged as a promising alternative to traditional silicon-based photovoltaics due to their lower material costs, flexibility, and potential for large-area deployment. Among various thin film technologies, copper indium gallium selenide (CIGS) solar cells have garnered significant attention for their high conversion efficiencies and stability. A critical component in these devices is the buffer layer, which typically consists of cadmium sulfide (CdS). This layer plays a pivotal role in optimizing the heterojunction interface, reducing recombination losses, and enhancing overall device performance. In this comprehensive review, I will delve into the fabrication of CdS buffer layers via chemical bath deposition (CBD), a prevalent method for producing high-quality thin films for CIGS thin film solar panels. I will explore the key parameters influencing film properties, elucidate the underlying reaction mechanisms, and discuss optimization strategies to improve the efficiency and scalability of these solar panels. Throughout this discussion, the importance of CdS in thin film solar panels will be emphasized, as it directly impacts the performance and commercial viability of CIGS-based devices.
CdS is an n-type semiconductor with a direct bandgap of approximately 2.42 eV, making it an excellent window layer material for thin film solar panels. Its primary function in CIGS solar cells is to form a heterojunction with the p-type CIGS absorber layer, facilitating charge carrier separation and collection. The quality of the CdS film—including its thickness, uniformity, crystallinity, and optical properties—profoundly affects the solar cell’s short-circuit current, open-circuit voltage, and fill factor. Therefore, mastering the deposition process is essential for manufacturing high-performance thin film solar panels. Chemical bath deposition is favored due to its simplicity, low cost, and ability to produce uniform films over large substrates. However, the process is sensitive to various parameters, which I will systematically analyze.
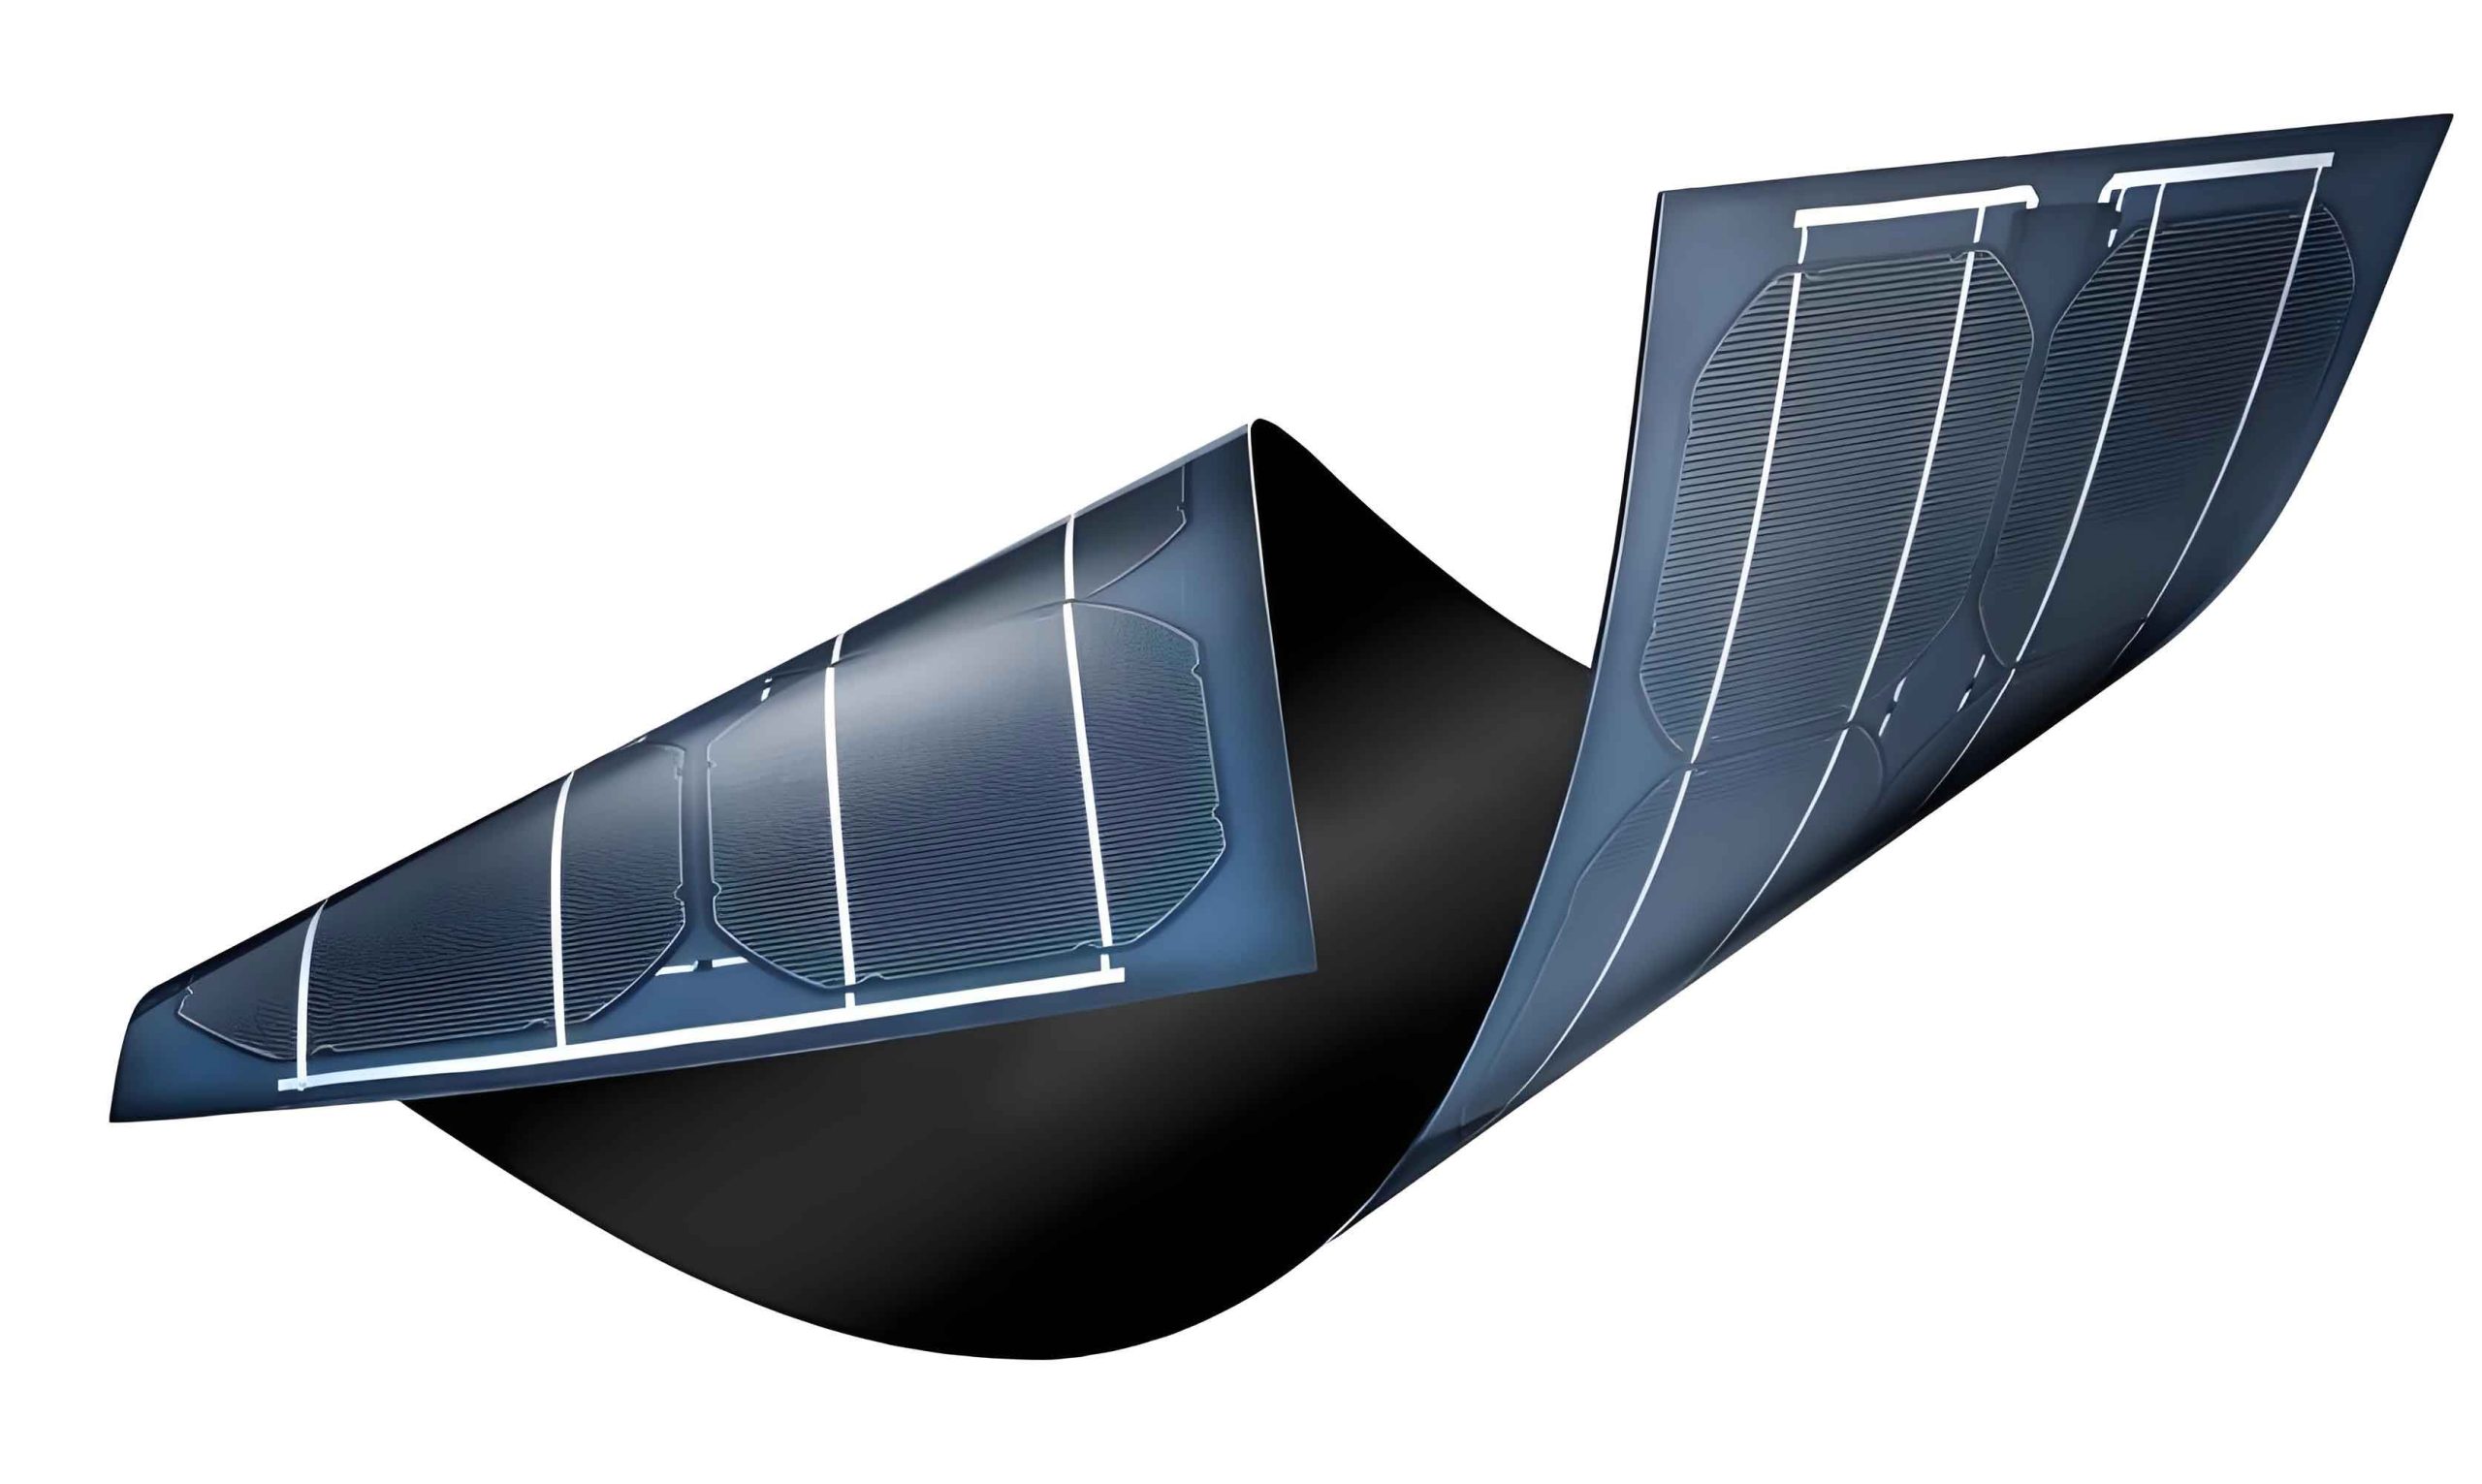
The deposition of CdS via CBD involves the controlled precipitation of CdS from an aqueous solution containing cadmium salts, sulfur sources (e.g., thiourea), and complexing agents (e.g., ammonia). The general reaction can be represented as:
$$ \text{Cd}^{2+} + \text{SC(NH}_2\text{)}_2 + 2\text{OH}^- \rightarrow \text{CdS} + \text{CN}_2\text{H}_2 + 2\text{H}_2\text{O} $$
In practice, the process is governed by a series of equilibrium reactions. The cadmium ions are complexed with ammonia to control their release rate, preventing rapid homogeneous precipitation. The complexation equilibrium is:
$$ \text{Cd}^{2+} + 4\text{NH}_3 \rightleftharpoons [\text{Cd(NH}_3\text{)}_4]^{2+} $$
Meanwhile, thiourea decomposes in alkaline medium to release sulfide ions:
$$ \text{SC(NH}_2\text{)}_2 + 2\text{OH}^- \rightarrow \text{S}^{2-} + \text{CN}_2\text{H}_2 + 2\text{H}_2\text{O} $$
The subsequent reaction between cadmium complexes and sulfide ions leads to CdS formation, either homogeneously in solution or heterogeneously on the substrate surface. The heterogeneous reaction is preferred for obtaining adherent, dense films suitable for thin film solar panels. The overall kinetics can be modeled using the following rate equation, where [Cd] and [S] represent the concentrations of active cadmium and sulfide species, respectively:
$$ \frac{d[\text{CdS}]}{dt} = k [\text{Cd}]^a [\text{S}]^b $$
Here, \( k \) is the rate constant, and \( a \) and \( b \) are reaction orders dependent on specific conditions. Understanding these fundamentals is crucial for manipulating deposition parameters to achieve optimal film properties for thin film solar panels.
Influencing Factors on CdS Film Properties
The quality of CdS buffer layers in thin film solar panels is highly sensitive to deposition conditions. I will examine four critical factors: precursor concentration, solution pH, bath temperature, and deposition time. Each factor influences film morphology, optical characteristics, and electrical performance, ultimately affecting the efficiency of CIGS thin film solar panels.
1. Precursor Concentration
The concentrations of cadmium source (e.g., cadmium acetate or cadmium sulfate) and sulfur source (thiourea) dictate the supersaturation level in the bath, which controls nucleation and growth kinetics. Higher concentrations generally increase deposition rates but may lead to non-uniform films if not properly balanced. Studies indicate that an optimal molar ratio of Cd:S around 1:1 to 1:3 yields films with good stoichiometry. For instance, increasing thiourea concentration enhances the cubic phase formation in CdS, which is beneficial for thin film solar panels due to its favorable band alignment with CIGS. The effect of concentration on film thickness \( d \) can be approximated by:
$$ d \propto C_{\text{Cd}} \cdot C_{\text{S}} \cdot t $$
where \( C_{\text{Cd}} \) and \( C_{\text{S}} \) are the concentrations of cadmium and sulfur precursors, and \( t \) is deposition time. However, excessive concentration can cause homogeneous nucleation, resulting in powdery deposits. The table below summarizes the impact of concentration variations on CdS films for thin film solar panels:
| Concentration Parameter | Low Range | Optimal Range | High Range | Effect on CdS Film |
|---|---|---|---|---|
| Cadmium Ion ([Cd²⁺]) | < 0.01 M | 0.01–0.05 M | > 0.05 M | Low: Incomplete coverage; Optimal: Uniform growth; High: Rough, porous film |
| Thiourea ([SC(NH₂)₂]) | < 0.02 M | 0.02–0.10 M | > 0.10 M | Low: Sulfur-deficient; Optimal: Stoichiometric CdS; High: Excess sulfur, reduced adhesion |
| Ammonia ([NH₃]) | < 0.5 M | 0.5–2.0 M | > 2.0 M | Low: Rapid precipitation; Optimal: Controlled release; High: Inhibited deposition |
Ammonia concentration is particularly crucial as it acts as a complexing agent. An optimal level ensures a balance between Cd²⁺ release and sulfide generation, promoting heterogeneous nucleation. This balance is vital for producing dense, pinhole-free films that enhance the performance of thin film solar panels.
2. Solution pH Value
The pH of the deposition bath profoundly affects the decomposition rate of thiourea and the stability of cadmium complexes. Typically, CBD of CdS is conducted in alkaline conditions (pH 9–12). At lower pH, thiourea decomposition is slow, leading to sulfur-deficient films, while excessively high pH may cause ammonia loss and uncontrolled precipitation. Research shows that a pH around 11.5 maximizes film density and optical transmittance. The pH dependence can be described by the following relationship for thiourea decomposition rate \( r_{\text{S}} \):
$$ r_{\text{S}} = k_{\text{pH}} [\text{OH}^-]^n $$
where \( k_{\text{pH}} \) is a pH-dependent constant, and \( n \) is typically between 1 and 2. Moreover, pH influences the crystalline phase of CdS. As pH increases, the film transitions from hexagonal to cubic phase, with the cubic phase being more desirable for thin film solar panels due to its lower lattice mismatch with CIGS. The phase transition can be correlated with the solution’s ionic product \( Q \) relative to the solubility product \( K_{\text{sp}} \) of CdS:
$$ Q = [\text{Cd}^{2+}][\text{S}^{2-}] $$
When \( Q > K_{\text{sp}} \), precipitation occurs, and the phase depends on the supersaturation ratio \( S = Q/K_{\text{sp}} \). At high pH, \( S \) favors cubic nucleation. The table below outlines pH effects:
| pH Range | Crystalline Phase | Transmittance (at 550 nm) | Bandgap (eV) | Suitability for Thin Film Solar Panels |
|---|---|---|---|---|
| 8.5–10.0 | Hexagonal dominant | 70–80% | 2.42–2.45 | Moderate: Higher interface defects |
| 10.5–11.5 | Mixed hexagonal/cubic | 80–85% | 2.40–2.42 | Good: Balanced properties |
| 11.5–12.0 | Cubic dominant | 85–90% | 2.38–2.40 | Excellent: Optimal for high-efficiency devices |
Thus, precise pH control is imperative for fabricating high-quality buffer layers that maximize the output of thin film solar panels.
3. Bath Temperature
Temperature governs the kinetic energy of reactants, influencing reaction rates, nucleation density, and film morphology. Generally, higher temperatures accelerate thiourea decomposition and CdS precipitation, leading to faster deposition. However, excessively high temperatures can promote homogeneous nucleation, causing coarse films. The optimal temperature range for CBD-CdS is 75–85°C. The temperature dependence follows the Arrhenius equation:
$$ k = A \exp\left(-\frac{E_a}{RT}\right) $$
where \( k \) is the rate constant, \( A \) is the pre-exponential factor, \( E_a \) is the activation energy (typically 40–60 kJ/mol for CBD-CdS), \( R \) is the gas constant, and \( T \) is absolute temperature. At temperatures near 85°C, heterogeneous nucleation dominates, yielding dense films with minimal voids. Conversely, below 70°C, films may be thin and non-uniform, while above 90°C, excessive grain growth occurs, increasing surface roughness. This roughness can scatter light and increase recombination in thin film solar panels. The effect of temperature on film thickness \( d \) over time \( t \) can be modeled as:
$$ d(T) = \int_0^t v(T) \, dt \quad \text{with} \quad v(T) = v_0 \exp\left(-\frac{E_v}{RT}\right) $$
where \( v(T) \) is the deposition velocity, and \( E_v \) is an empirical activation energy for growth. Below is a summary of temperature effects:
| Temperature Range (°C) | Deposition Rate (nm/min) | Film Morphology | Grain Size (nm) | Impact on Thin Film Solar Panels |
|---|---|---|---|---|
| 60–70 | 2–5 | Patchy, incomplete | 10–20 | Poor: Low fill factor due to shunts |
| 75–85 | 5–10 | Dense, smooth | 20–50 | Optimal: High efficiency and stability |
| 85–95 | 10–15 | Rough, porous | 50–100 | Suboptimal: Increased recombination |
Therefore, maintaining a stable bath temperature is critical for reproducible CdS buffer layers in thin film solar panels.
4. Deposition Time
Deposition time directly controls film thickness, which is a key parameter in thin film solar panels. Thicker films may reduce optical transmission, while thinner films might not fully cover the absorber layer, leading to shunts. The ideal thickness for CdS in CIGS solar cells is 50–100 nm. During CBD, film growth often follows a two-stage process: an initial linear regime where heterogeneous nucleation dominates, followed by a saturation regime where homogeneous precipitation contributes to surface roughness. The thickness \( d \) as a function of time \( t \) can be expressed as:
$$ d(t) = d_{\infty} \left(1 – \exp(-kt)\right) $$
where \( d_{\infty} \) is the asymptotic thickness, and \( k \) is a rate constant. Studies show that at around 30–40 minutes, films achieve optimal thickness with high transmittance (>80%) and minimal defects. Prolonged deposition increases thickness but can also alter stoichiometry, as indicated by the Cd/S atomic ratio measured by EDX. This ratio affects the bandgap \( E_g \) via the empirical relation:
$$ E_g = E_{g0} + \alpha \cdot \Delta(\text{Cd/S}) $$
where \( E_{g0} \) is the bandgap of stoichiometric CdS (2.42 eV), \( \alpha \) is a constant, and \( \Delta(\text{Cd/S}) \) is the deviation from unity. The table below illustrates time-dependent properties:
| Deposition Time (min) | Thickness (nm) | Transmittance (%) | Cd/S Atomic Ratio | Bandgap (eV) | Performance in Thin Film Solar Panels |
|---|---|---|---|---|---|
| 10–20 | 20–40 | 85–90 | 0.9–1.0 | 2.43–2.45 | Insufficient buffer, high \( J_{sc} \) but low \( V_{oc} \) |
| 30–40 | 50–80 | 80–85 | 1.0–1.1 | 2.40–2.42 | Optimal: Balanced \( J_{sc} \) and \( V_{oc} \), high efficiency |
| 50–60 | 90–120 | 70–75 | 1.1–1.3 | 2.38–2.40 | Reduced current due to absorption losses |
Thus, precise timing is essential to tailor the buffer layer for maximum performance in thin film solar panels.
Chemical Bath Deposition Methodology and Reaction Mechanisms
Having analyzed the influencing factors, I now detail the CBD process for CdS buffer layers, which is central to manufacturing CIGS thin film solar panels. The typical CBD setup involves a temperature-controlled bath containing the reaction solution and substrates immersed vertically or horizontally. The substrates, often glass or CIGS-coated molybdenum, are pre-cleaned to ensure adhesion. The solution composition includes a cadmium salt (e.g., 0.01 M cadmium acetate), thiourea (0.05 M), ammonia (1–2 M), and sometimes ammonium salts as buffers. The deposition proceeds via two competing pathways: heterogeneous and homogeneous reactions.
The heterogeneous reaction occurs at the substrate surface, where CdS nuclei form directly, leading to a dense film. This process is favored by moderate supersaturation, achieved through optimal concentration, pH, and temperature. The rate of heterogeneous nucleation \( J_{\text{het}} \) can be described by classical nucleation theory:
$$ J_{\text{het}} = A_{\text{het}} \exp\left(-\frac{\Delta G_{\text{het}}^*}{kT}\right) $$
where \( A_{\text{het}} \) is a pre-factor, \( \Delta G_{\text{het}}^* \) is the critical Gibbs free energy for heterogeneous nucleation, \( k \) is Boltzmann’s constant, and \( T \) is temperature. For thin film solar panels, maximizing \( J_{\text{het}} \) relative to homogeneous nucleation ensures smooth, adherent films.
Homogeneous reaction, in contrast, occurs in the bulk solution, generating CdS colloids that may adsorb onto the film, causing roughness. This mechanism dominates at high supersaturation or prolonged times. The rate \( J_{\text{hom}} \) is given by:
$$ J_{\text{hom}} = A_{\text{hom}} \exp\left(-\frac{\Delta G_{\text{hom}}^*}{kT}\right) $$
with \( \Delta G_{\text{hom}}^* > \Delta G_{\text{het}}^* \). To favor heterogeneous growth, parameters are tuned to maintain \( Q \) slightly above \( K_{\text{sp}} \). The interplay between these mechanisms dictates film quality. Practically, the process involves the following steps:
- Solution Preparation: Dissolve cadmium acetate in deionized water, add ammonia under stirring to form the complex, then introduce thiourea. Adjust pH with ammonium hydroxide or acetic acid.
- Substrate Immersion: Place substrates in the bath after solution reaches desired temperature (e.g., 80°C).
- Deposition: Allow reaction to proceed for a set time (e.g., 30 min), during which the solution changes from clear to yellow due to CdS formation.
- Termination and Cleaning: Remove substrates, rinse with deionized water to stop reaction, and dry in nitrogen.
The resulting CdS film is typically characterized using techniques like XRD, SEM, UV-Vis spectroscopy, and Hall effect measurements to assess crystallinity, morphology, optical properties, and electrical conductivity—all critical for integration into thin film solar panels.
To optimize the process for thin film solar panels, advanced strategies have been explored. For instance, using alternative complexing agents like triethanolamine can offer better control over cadmium release. Additionally, post-deposition annealing in air or inert atmospheres can improve crystallinity and reduce defects. The annealing effect on carrier concentration \( n \) can be modeled as:
$$ n = n_0 \exp\left(-\frac{E_a}{kT}\right) $$
where \( n_0 \) is the initial concentration and \( E_a \) is activation energy for defect passivation. Moreover, doping CdS with elements like indium or zinc can enhance conductivity and band alignment, further boosting the efficiency of thin film solar panels.
Future Directions and Challenges
While CBD-CdS remains the standard for high-efficiency CIGS thin film solar panels, there are ongoing efforts to address its limitations. One major challenge is the use of toxic cadmium, prompting research into alternative buffer layers like ZnS, In₂S₃, or Zn₁₋ₓMgₓO. These materials aim to maintain performance while reducing environmental impact. Another area is the development of vacuum-based deposition methods (e.g., atomic layer deposition) that allow in-line processing without breaking vacuum, potentially increasing throughput for mass production of thin film solar panels. However, CBD still offers advantages in cost and simplicity for laboratory-scale and certain commercial applications.
Furthermore, optimizing CdS deposition for flexible substrates is crucial for emerging applications in building-integrated photovoltaics and portable electronics. This requires low-temperature processes (below 70°C) that retain film quality. Mathematical modeling can aid in predicting film properties under various conditions. For example, a comprehensive model integrating all factors might look like:
$$ \text{Film Quality Index } Q_f = f(C_{\text{Cd}}, C_{\text{S}}, \text{pH}, T, t) = \alpha \ln(C_{\text{Cd}}) + \beta \ln(C_{\text{S}}) + \gamma \text{pH} + \delta \frac{1}{T} + \epsilon t $$
where \( \alpha, \beta, \gamma, \delta, \epsilon \) are coefficients determined experimentally. Such models can streamline the optimization process for thin film solar panels.
In conclusion, the CdS buffer layer plays an indispensable role in CIGS thin film solar panels, and its deposition via chemical bath deposition is a nuanced process governed by multiple interrelated parameters. Through careful control of concentration, pH, temperature, and time, high-quality films can be achieved, leading to solar cells with efficiencies exceeding 20%. As research progresses, the integration of novel materials and processes will continue to push the boundaries of thin film solar panel technology, contributing to a sustainable energy future. The insights presented here underscore the importance of fundamental understanding and precise engineering in advancing photovoltaic devices.