
In recent years, the rapid adoption of renewable energy technologies has positioned thin film solar panels as a pivotal solution to global challenges such as climate change, energy depletion, and environmental pollution. Among these, cadmium telluride (CdTe) thin film solar panels have emerged as one of the most mature and commercially viable options due to their high efficiency and low production costs. However, the end-of-life management of these thin film solar panels presents significant environmental and resource concerns, primarily because they contain scarce tellurium (Te) and toxic cadmium (Cd). Native resources for these elements are limited and difficult to extract, and improper disposal can lead to severe contamination from heavy metals and organic adhesives. Therefore, developing efficient and environmentally friendly methods for recovering Te and Cd from waste CdTe thin film solar panels is crucial for sustainable resource utilization and pollution prevention.
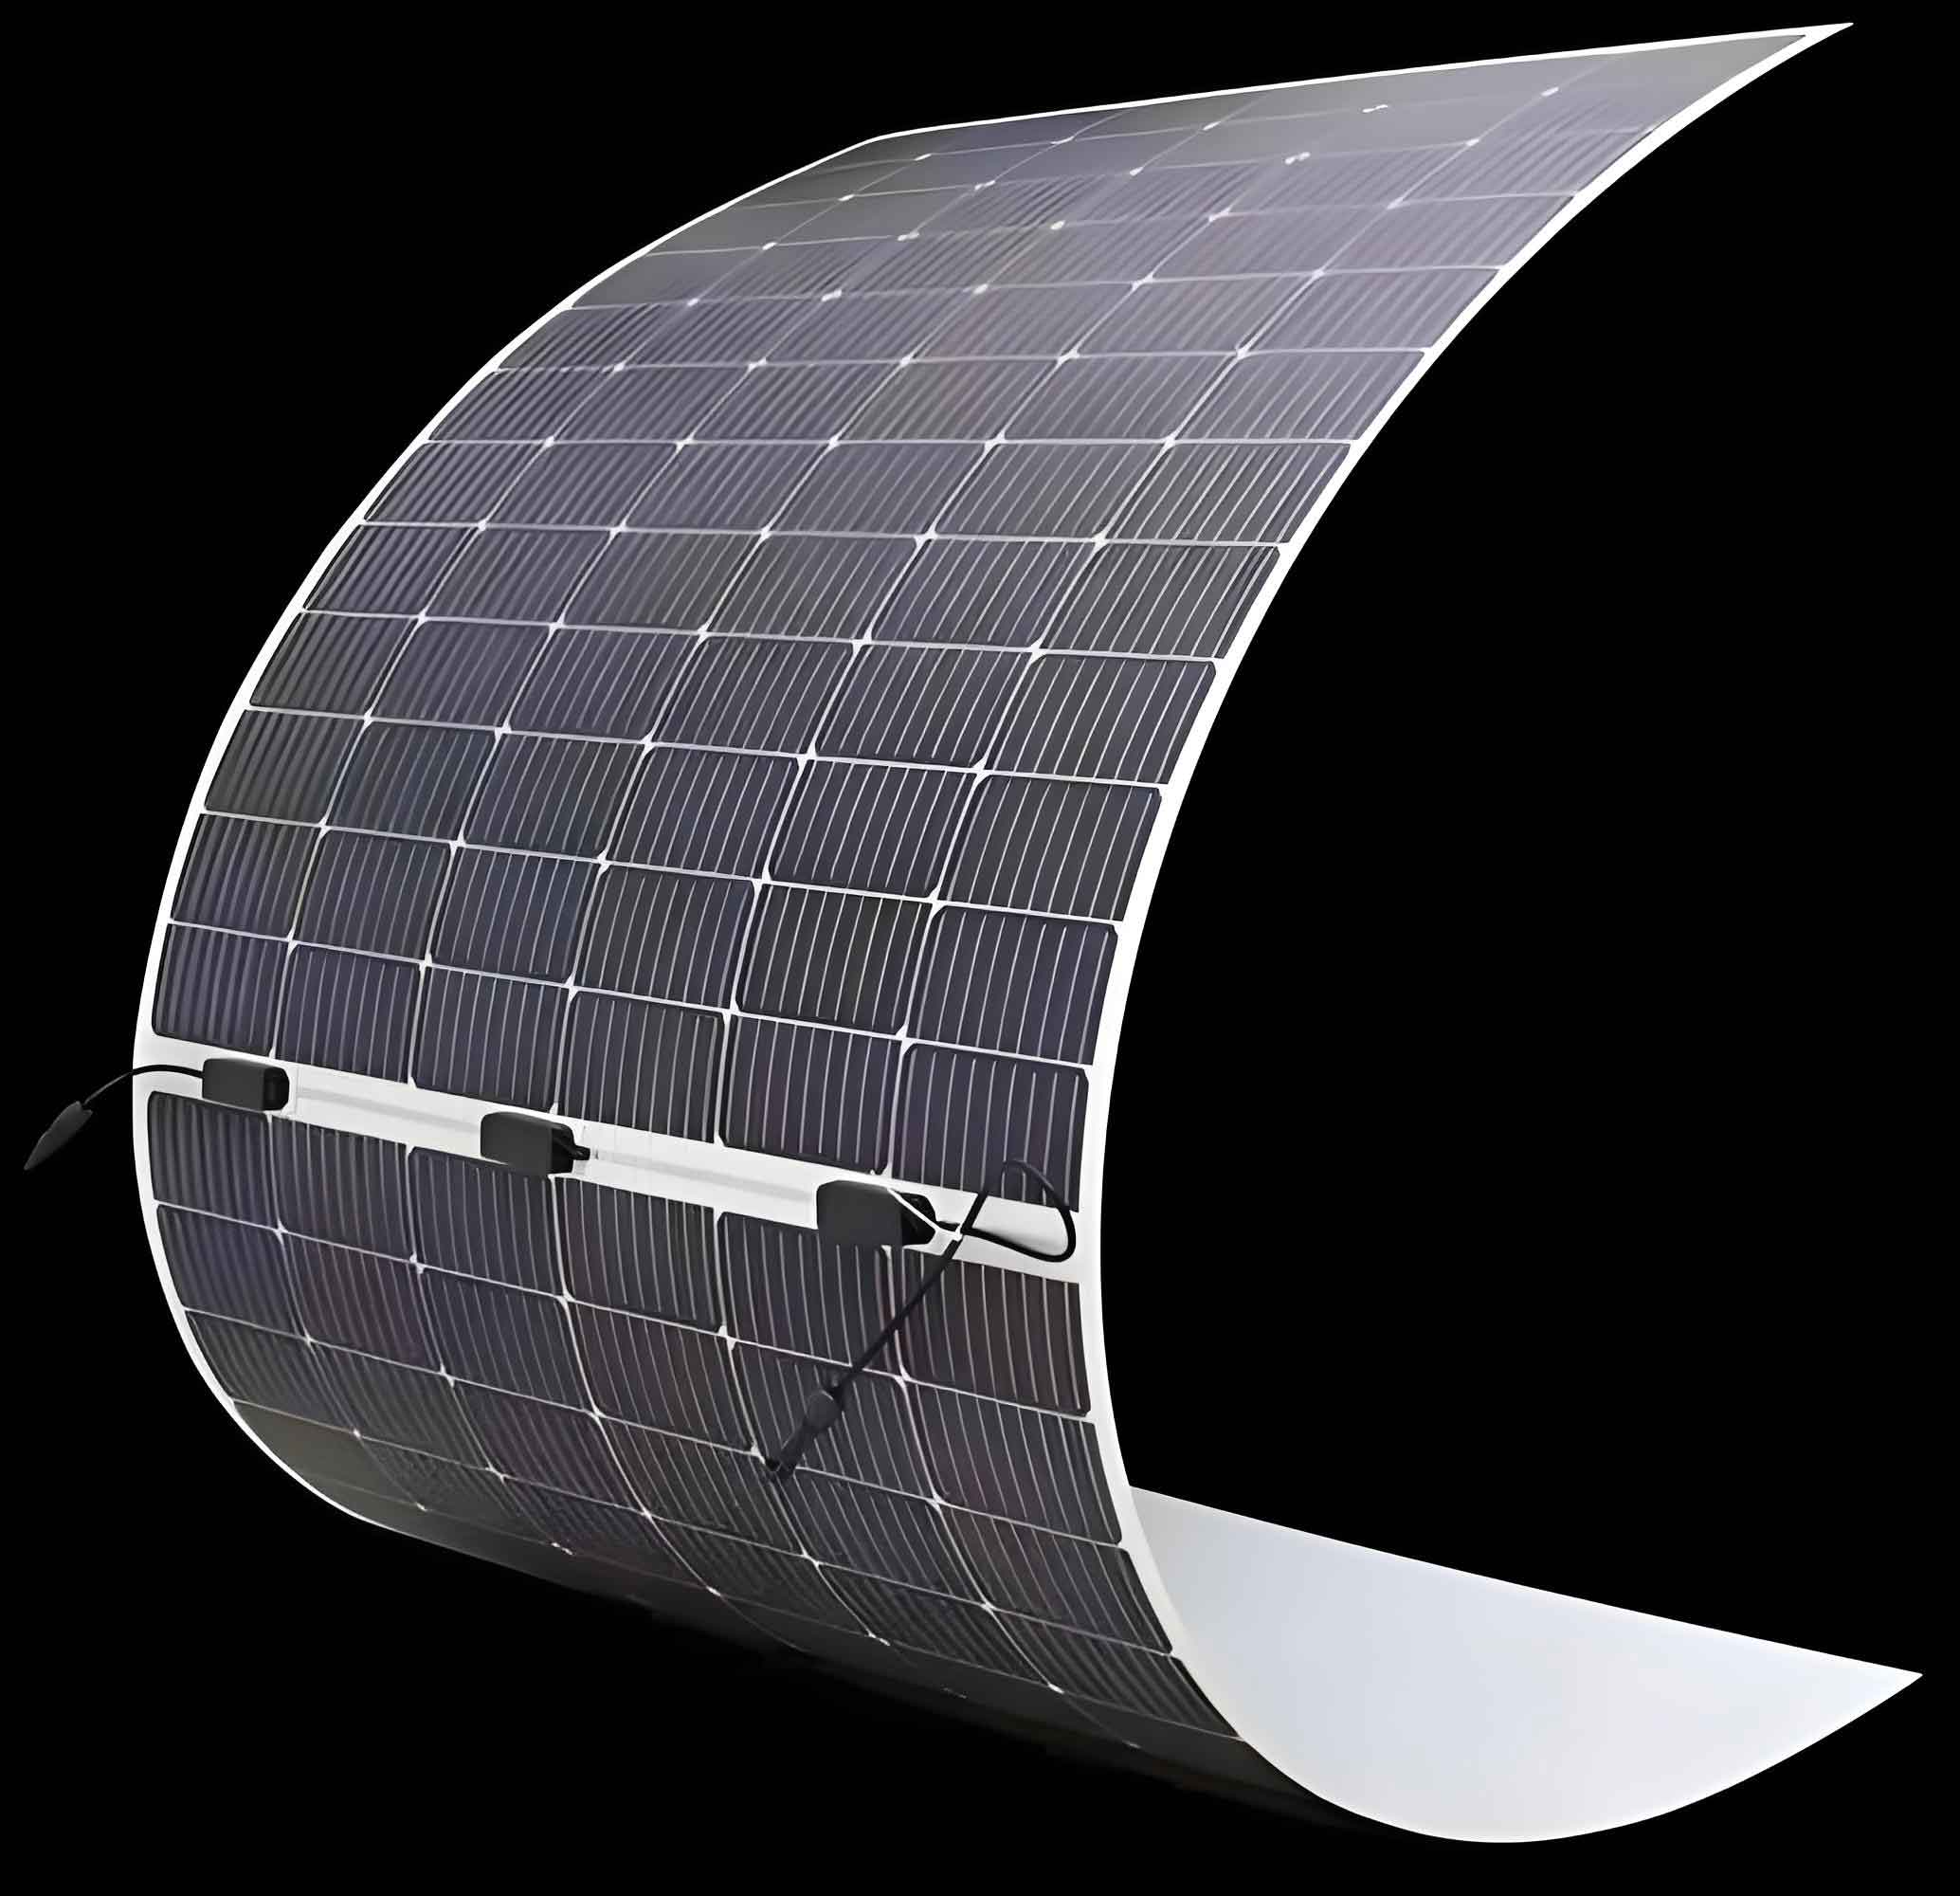
Current recycling processes for waste CdTe thin film solar panels can be broadly categorized into gaseous and liquid methods. Gaseous methods, such as vacuum distillation or pyrolysis, often require high operational conditions and involve substantial equipment investment and running costs. Liquid methods, including acid leaching or solvent extraction, tend to have simpler flows but suffer from lengthy processes, poor working conditions, generation of heavy metal wastewater, and high water consumption. To address these limitations, I have explored an alternative approach: oxidative roasting. This method leverages the unique properties of CdTe and its oxides, offering a simple, economical, and effective pathway for recovering Te and Cd from waste thin film solar panels while minimizing secondary pollution.
The core principle behind this method lies in the oxidative behavior of CdTe. Cadmium telluride is a black, high-density cubic crystalline compound that is insoluble in water. When exposed to air and moisture under heating, it can react with oxygen and water vapor to decompose. The oxidation reactions can be represented as follows:
$$ \text{CdTe} + \frac{3}{2}\text{O}_2 \rightarrow \text{CdO} + \text{TeO}_2 $$
Under certain conditions, especially in the presence of water vapor, the reaction may proceed as:
$$ \text{CdTe} + \text{O}_2 + \text{H}_2\text{O} \rightarrow \text{CdO} + \text{TeO}_2 + \text{H}_2 $$
Tellurium dioxide (TeO2) has a melting point of 733°C and sublimes readily above this temperature. Cadmium oxide (CdO) is a dark brown powder that begins to sublime around 700°C. By exploiting these characteristics—namely, the ease of oxidation of CdTe and the low melting points and sublimation tendencies of the resulting oxides—I designed an oxidative roasting process. In this process, waste CdTe thin film solar panels are heated in an oxidizing atmosphere, converting Te and Cd into their volatile oxides, which then enter the flue gas. These oxides can be subsequently captured through dust collection or condensation methods, enabling efficient recovery without generating liquid waste or complex by-products.
To optimize this process for industrial applications, I conducted a series of experiments to investigate the effects of key parameters, such as roasting temperature and time, on the recovery rates of Te and Cd. This study aims to provide a foundational framework for scaling up the recycling of thin film solar panels, contributing to the circular economy in the photovoltaic industry.
Experimental Materials and Methods
The experimental materials consisted of waste CdTe thin film solar panels sourced from a recycling facility. These panels typically comprise multiple layers, including glass substrates, ethylene-vinyl acetate (EVA) films, and the active CdTe layer. The initial step involved manual dismantling to remove the back glass and EVA films, followed by mechanical processing to obtain a homogeneous powder for roasting. Specifically, the panels were first broken into 2–4 cm pieces using a jaw crusher, then further reduced to under 1 cm with a disc mill, and finally ground into a fine powder using a mortar and pestle. This powder was subjected to fluorescence analysis to determine its elemental composition, as summarized in Table 1.
| Component | SiO2 | MnO | Na2O | MgO | Al2O3 | SO3 | Fe2O3 | K2O | TeO2 | CdO | Cl | Cr2O3 | TiO2 | SnO2 | P2O5 | MoO3 | ZnO | NiO | CaO |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Content | 68.45 | 0.01 | 9.83 | 3.08 | 1.46 | 0.38 | 0.35 | 0.28 | 0.17 | 0.16 | 0.11 | 0.11 | 0.08 | 0.06 | 0.02 | 0.02 | 0.01 | 0.01 | 15.4 |
From Table 1, it is evident that the powder is predominantly composed of silica (SiO2) and calcium oxide (CaO), which originate from the glass substrates. The tellurium and cadmium contents, expressed as their oxides, are relatively low (0.17% TeO2 and 0.16% CdO), highlighting the need for an efficient recovery process to extract these valuable elements from the bulk matrix. The corresponding elemental concentrations of Te and Cd were in the ranges of 920–1020 × 10−6 and 420–500 × 10−6, respectively.
The oxidative roasting experiments were performed in a high-temperature furnace equipped with a programmable temperature controller. For each trial, a measured quantity of the powder (typically 10–20 grams) was placed in an alumina crucible and inserted into the furnace. The atmosphere was ambient air, providing the necessary oxygen for oxidation. The furnace was heated to the desired temperature at a rate of 10°C/min, held for a specified duration, and then allowed to cool naturally. The resulting roasted product, referred to as calcine, was collected and analyzed for residual Te and Cd contents using inductively coupled plasma optical emission spectrometry (ICP-OES). The recovery rates (R) of Te and Cd were calculated using the formula:
$$ R(\%) = \left(1 – \frac{C_{\text{final}} \times W_{\text{final}}}{C_{\text{initial}} \times W_{\text{initial}}}\right) \times 100 $$
where \( C_{\text{initial}} \) and \( C_{\text{final}} \) are the concentrations of Te or Cd in the initial powder and calcine, respectively, and \( W_{\text{initial}} \) and \( W_{\text{final}} \) are the corresponding weights. To account for mass loss during roasting, primarily due to the sublimation of oxides and decomposition of organics, the weights were carefully measured before and after each experiment.
Influence of Roasting Temperature on Recovery Rates
The roasting temperature is a critical parameter that affects both the oxidation kinetics of CdTe and the sublimation behavior of TeO2 and CdO. To establish an appropriate temperature range, I conducted preliminary experiments at various temperatures, from 400°C to 1300°C, with a fixed roasting time of 30 minutes. These trials also aimed to observe the behavior of the EVA film and glass components, which are integral parts of thin film solar panels.
At 400°C, the EVA film began to decompose, but the glass showed no signs of softening. By 450°C, the EVA film was completely decomposed, and the glass exhibited slight softening. At 500°C, the glass fully softened, and at 600°C, it formed a molten mass. These observations indicate that temperatures above 500°C are sufficient to degrade the organic components and melt the glass, which may facilitate the release of CdTe from the matrix. However, excessive temperatures, such as 1300°C, lead to complete glass melting but also increase energy consumption unnecessarily. A fluorescence analysis of the calcine obtained at 1300°C for 30 minutes revealed significant reductions in TeO2 and CdO contents, as shown in Table 2.
| Component | SiO2 | MnO | Na2O | MgO | Al2O3 | SO3 | Fe2O3 | CaO | TeO2 | CdO | Cl | Cr2O3 | TiO2 | SnO2 | P2O5 | MoO3 | ZnO | NiO | Te | Cd |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Content | 70.38 | 0.01 | 11.04 | 3.37 | 1.72 | 0.14 | 0.37 | 12.41 | 0.03 | 0.09 | 0.08 | 0.11 | 0.08 | 0.03 | 0.03 | 0.04 | 0.01 | 0.09 | 0.0960 | 0.0438 |
In Table 2, the TeO2 and CdO contents dropped to 0.03% and 0.09%, respectively, suggesting effective sublimation. However, to optimize energy efficiency, I focused on lower temperatures. Based on the sublimation points of TeO2 (733°C) and CdO (700°C), I selected a range of 600°C to 800°C for detailed study, with a roasting time of 30 minutes. The residual TeO2 and CdO contents in the calcine are presented in Table 3.
| Roasting Temperature (°C) | Roasting Time (min) | CdO Content (%) | TeO2 Content (%) |
|---|---|---|---|
| 600 | 30 | 0.06 | 0.05 |
| 650 | 30 | 0.05 | 0.03 |
| 750 | 30 | 0.03 | 0.02 |
| 800 | 30 | 0.03 | 0.02 |
From Table 3, it is clear that as the temperature increases from 600°C to 750°C, the residual contents of both TeO2 and CdO decrease, indicating higher recovery rates. This trend aligns with the enhanced oxidation and sublimation at elevated temperatures. The data can be modeled using an Arrhenius-type equation for the sublimation rate constant \( k \):
$$ k = A \exp\left(-\frac{E_a}{RT}\right) $$
where \( A \) is the pre-exponential factor, \( E_a \) is the activation energy, \( R \) is the gas constant, and \( T \) is the absolute temperature. The reduction in residual content with temperature suggests that the process is thermally activated. However, between 750°C and 800°C, the residual contents plateau, implying that further temperature increases yield diminishing returns. This may be due to the complete oxidation of available CdTe or equilibrium limitations in the sublimation process. Therefore, from an energy-saving perspective, 750°C was chosen as the optimal temperature for subsequent experiments.
Influence of Roasting Time on Recovery Rates
After determining the optimal temperature, I investigated the effect of roasting time on recovery rates. Holding the temperature constant at 750°C, I varied the roasting time from 30 to 90 minutes. The residual TeO2 and CdO contents in the calcine are summarized in Table 4.
| Roasting Temperature (°C) | Roasting Time (min) | CdO Content (%) | TeO2 Content (%) |
|---|---|---|---|
| 750 | 30 | 0.033 | 0.024 |
| 750 | 60 | 0.029 | 0.021 |
| 750 | 90 | 0.027 | 0.019 |
The data in Table 4 show that extending the roasting time from 30 to 90 minutes leads to a gradual decrease in residual TeO2 and CdO contents, but the rate of decrease diminishes over time. For instance, the reduction in CdO content from 30 to 60 minutes is 0.004%, whereas from 60 to 90 minutes, it is only 0.002%. This behavior can be described by a first-order kinetic model for the sublimation process:
$$ \frac{dC}{dt} = -kC $$
where \( C \) is the concentration of the oxide in the solid, and \( k \) is the rate constant. Integrating this equation gives:
$$ \ln\left(\frac{C_0}{C}\right) = kt $$
where \( C_0 \) is the initial concentration. Plotting \(\ln(C_0/C)\) versus time would yield a straight line if the model holds, but the diminishing returns suggest that factors such as diffusion limitations or changes in the solid matrix (e.g., glass melting) may complicate the kinetics. Nonetheless, to balance recovery efficiency with operational throughput, a roasting time of 60 minutes was selected as optimal, as it achieves substantial recovery without excessive energy input.
Comprehensive Condition Experiments and Recovery Rate Calculations
Based on the above findings, I conducted comprehensive experiments under the optimized conditions: roasting temperature of 750°C and roasting time of 60 minutes. The calcine obtained was analyzed for residual Te and Cd contents, and the recovery rates were calculated. The results are presented in Table 5.
| Parameter | CdO Content (%) | TeO2 Content (%) | Te Content (×10−6) | Cd Content (×10−6) | Recovery Rate (%) |
|---|---|---|---|---|---|
| Calcine | 0.029 | 0.021 | 58 | 47 | – |
| Te Recovery | – | – | – | – | 93.96 |
| Cd Recovery | – | – | – | – | 89.27 |
The recovery rates of 93.96% for Te and 89.27% for Cd demonstrate the effectiveness of the oxidative roasting method. These high yields are attributable to the complete oxidation of CdTe and efficient sublimation of the oxides at 750°C. The slightly lower recovery for Cd may be due to partial retention in the glass melt or formation of non-volatile compounds. Nonetheless, these results surpass many traditional liquid-based methods and avoid the generation of hazardous wastewater, making this approach environmentally benign.
To further contextualize these results, I compared the energy consumption of this method with other recycling processes for thin film solar panels. Assuming an industrial-scale setup with heat recovery, the energy required for roasting at 750°C can be estimated using the specific heat capacities of the materials. For a batch containing 1 ton of waste thin film solar panel powder, the energy input \( Q \) can be approximated as:
$$ Q = m \int_{T_0}^{T_f} C_p(T) \, dT $$
where \( m \) is the mass, \( C_p(T) \) is the temperature-dependent heat capacity, \( T_0 \) is room temperature (25°C), and \( T_f \) is the roasting temperature (750°C). Using average values for glass and metal oxides, \( Q \) is roughly 500–600 MJ per ton, which is comparable to or lower than the energy required for acid leaching and wastewater treatment in liquid methods.
Mechanistic Insights and Environmental Implications
The success of oxidative roasting hinges on the physicochemical transformations of CdTe. During heating, CdTe first oxidizes to CdO and TeO2. These oxides then sublime and are carried away by the gas stream. The sublimation process can be described by the vapor pressure equations for TeO2 and CdO. For TeO2, the vapor pressure \( P \) as a function of temperature \( T \) is given by:
$$ \log_{10}(P/\text{atm}) = A – \frac{B}{T} $$
where \( A \) and \( B \) are constants derived from experimental data. Similar equations exist for CdO. At 750°C, the vapor pressures are sufficiently high to ensure rapid sublimation, especially in a flowing air atmosphere that removes the vapors from the equilibrium.
An important aspect of this method is its handling of the EVA film and other organics present in thin film solar panels. During roasting, these organics decompose into volatile gases such as carbon dioxide and water vapor, which are innocuous when released in controlled conditions. This eliminates the need for separate organic removal steps, simplifying the process. Moreover, the glass matrix melts and forms an inert slag that can potentially be repurposed in construction materials, adding to the sustainability of the method.
From an environmental perspective, oxidative roasting avoids the secondary pollution commonly associated with liquid methods. Traditional hydrometallurgical approaches generate acidic or alkaline wastewaters containing heavy metals, requiring extensive treatment. In contrast, the gaseous emissions from roasting primarily consist of TeO2 and CdO vapors, which can be effectively captured using bag filters or electrostatic precipitators. The collected oxide dust is then a direct feedstock for tellurium and cadmium refining. This closed-loop approach minimizes environmental release and aligns with green chemistry principles.
Scalability and Industrial Application Potential
To assess the scalability of this method, I considered key engineering parameters such as throughput, equipment design, and cost. A continuous rotary kiln or fluidized bed reactor could be employed for large-scale processing of waste thin film solar panels. The roasting temperature of 750°C is well within the operational range of standard industrial furnaces. The retention time of 60 minutes allows for adequate oxidation and sublimation, and the process can be optimized further by adjusting the air flow rate to enhance mass transfer.
The economic viability depends on the recovery rates and the market prices of Te and Cd. Tellurium is a rare element with applications in semiconductors and thermoelectrics, commanding a high price. Cadmium, though less valuable, is critical for nickel-cadmium batteries and coatings. The recovery rates achieved here (over 90% for Te and nearly 90% for Cd) ensure a positive return on investment, especially when combined with the low operational costs of roasting compared to wet chemistry methods.
Furthermore, this method contributes to the circular economy by enabling the reuse of critical materials from end-of-life thin film solar panels. As the deployment of thin film solar panels continues to grow, establishing efficient recycling infrastructure is essential to mitigate resource scarcity and environmental impacts. The oxidative roasting process offers a robust solution that can be integrated into existing metallurgical facilities, leveraging their expertise in high-temperature processing.
Conclusion and Future Directions
In this study, I have demonstrated that oxidative roasting is a highly effective method for recovering tellurium and cadmium from waste cadmium telluride thin film solar panels. The optimal conditions—roasting temperature of 750°C and time of 60 minutes—yield recovery rates of 93.96% for Te and 89.27% for Cd. This process capitalizes on the oxidative and sublimation properties of CdTe and its oxides, offering a simple, economical, and environmentally friendly alternative to conventional recycling techniques. By avoiding liquid waste and minimizing secondary pollution, it addresses key challenges in the sustainable management of thin film solar panel waste.
Future research could explore several avenues to enhance this method. First, investigating the effects of atmosphere composition, such as adding steam or controlled oxygen levels, might improve oxidation kinetics and recovery yields. Second, integrating real-time monitoring techniques, like thermogravimetric analysis coupled with mass spectrometry, could provide deeper insights into the reaction mechanisms. Third, scaling up to pilot-scale trials would validate the technical and economic feasibility for industrial adoption. Additionally, extending this approach to other types of thin film solar panels, such as copper indium gallium selenide (CIGS), could broaden its applicability.
In summary, the oxidative roasting method represents a significant step forward in the recycling of thin film solar panels. It not only recovers valuable resources but also supports the environmental sustainability of the photovoltaic industry. As the world transitions to renewable energy, developing efficient recycling technologies for thin film solar panels will be crucial in closing the material loop and promoting a circular economy.