
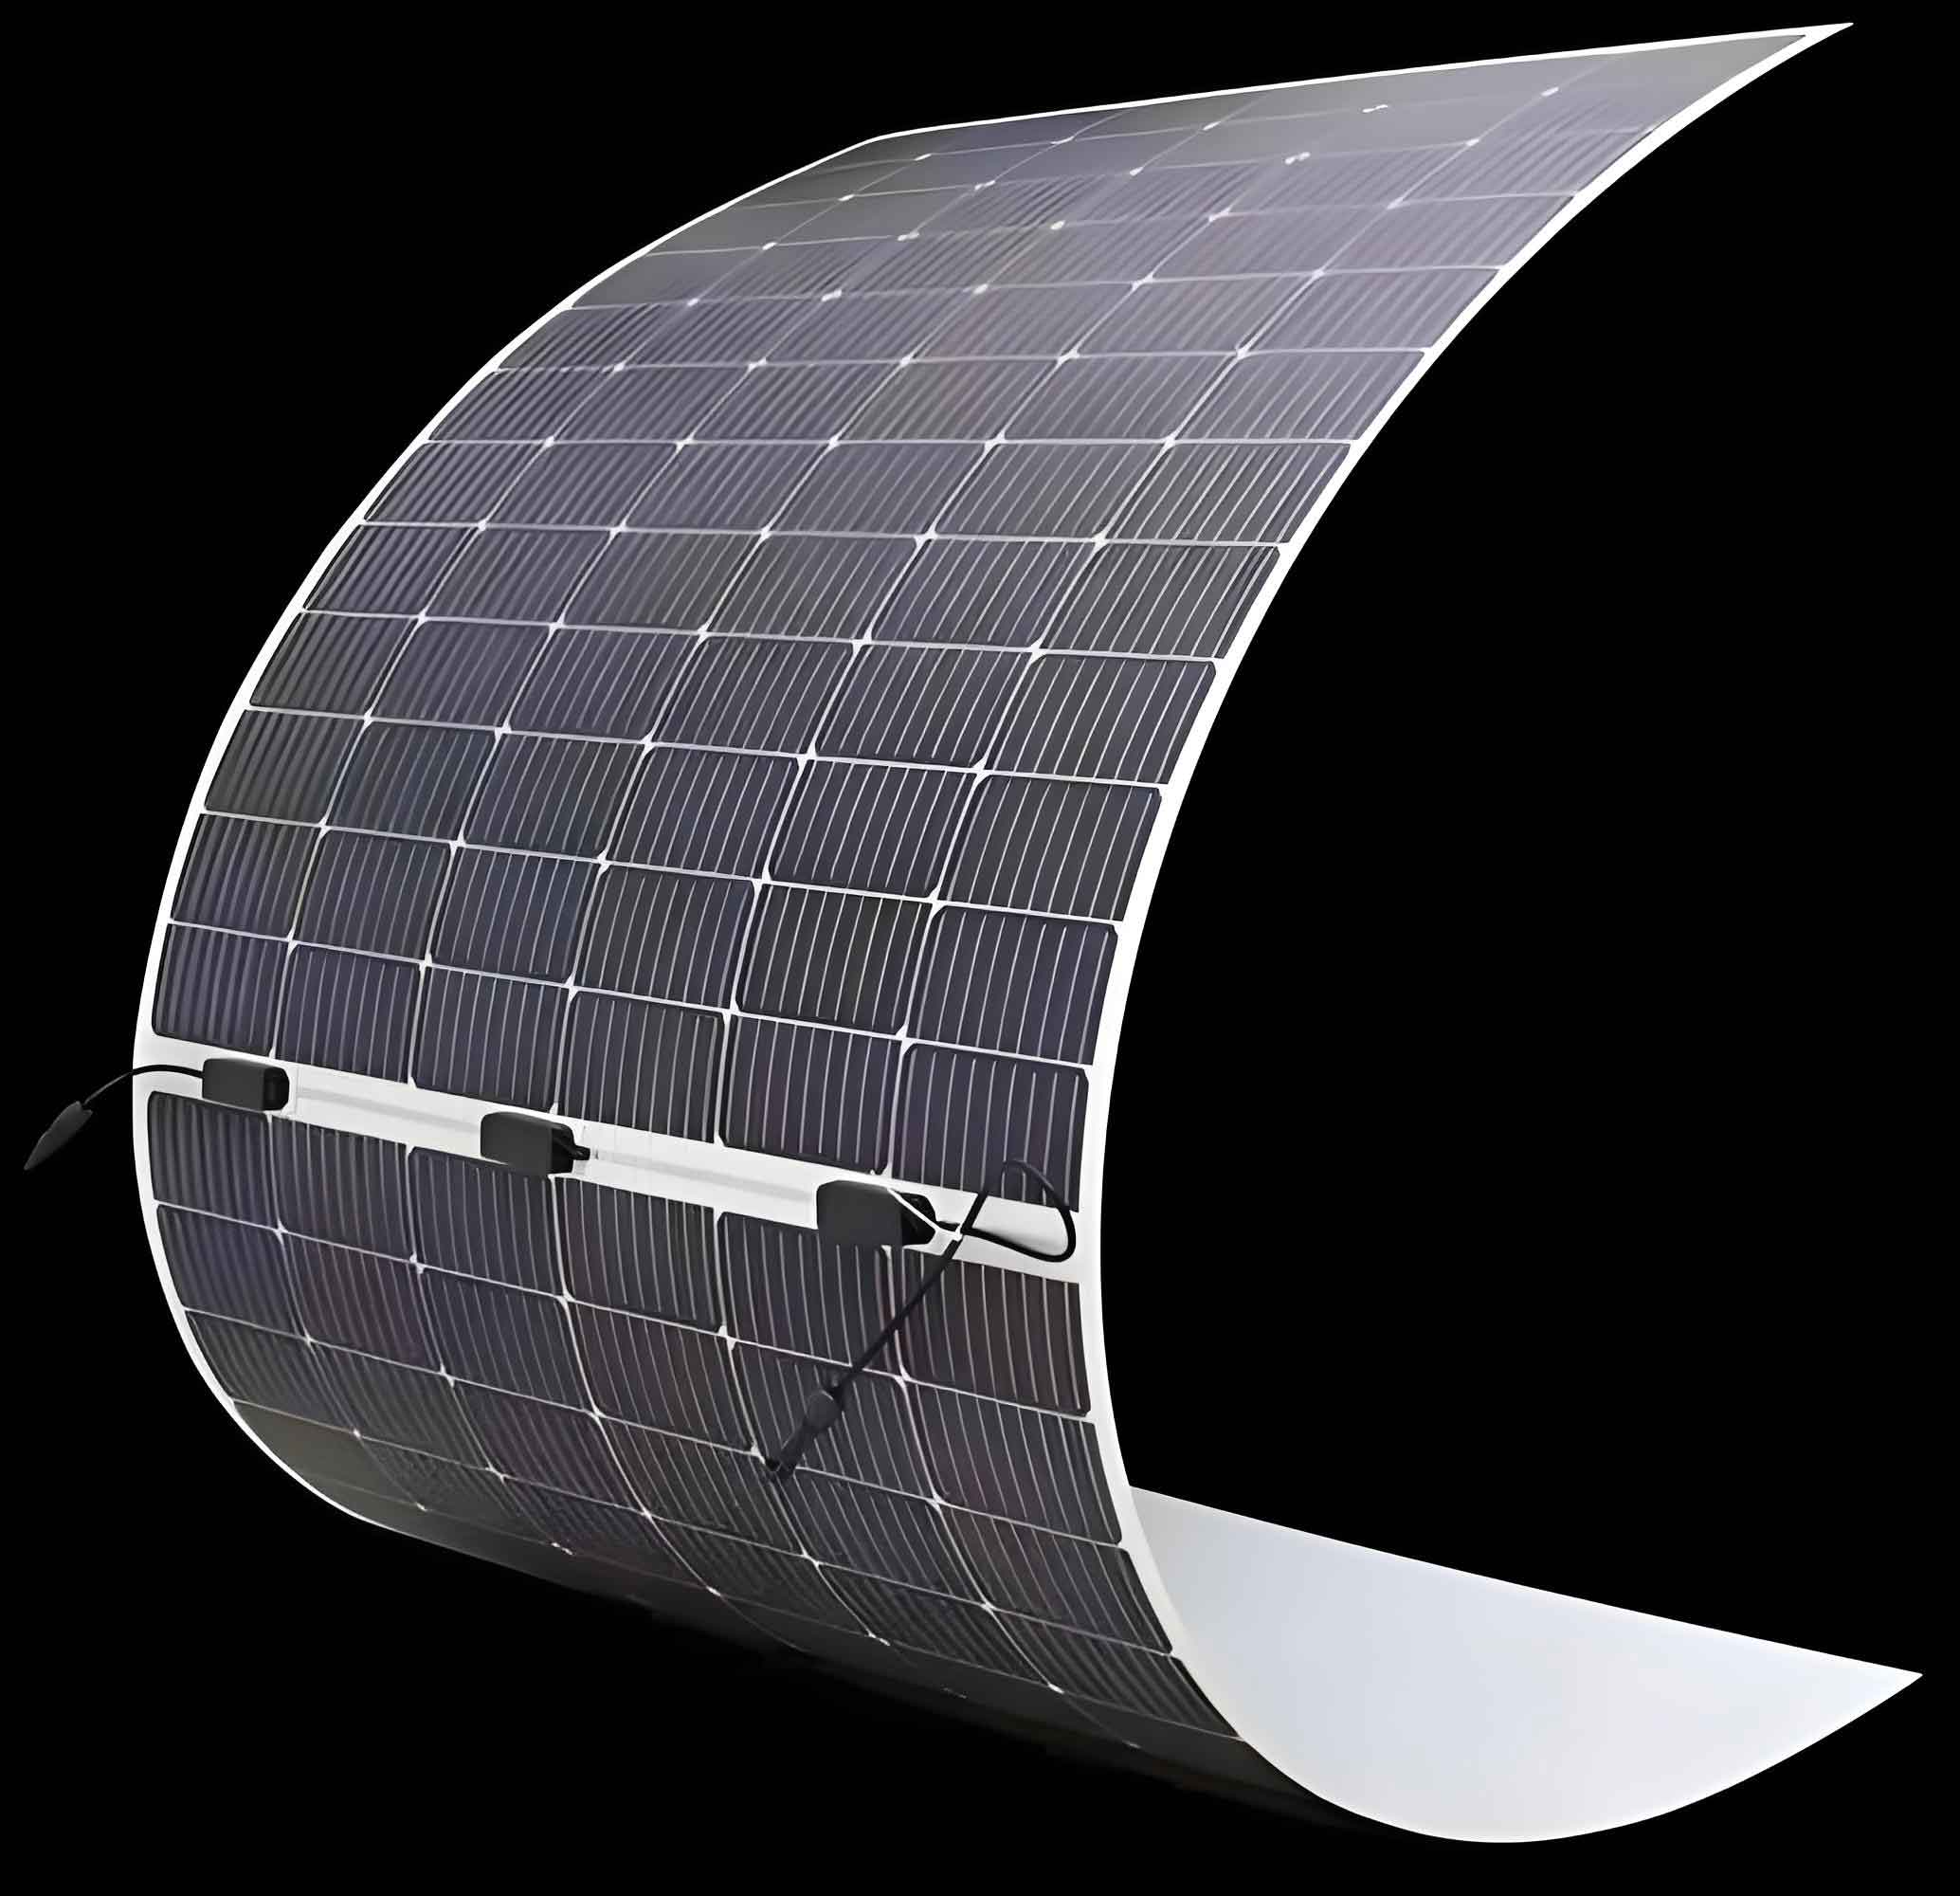
The relentless global demand for energy, coupled with the urgent need to mitigate climate change, has propelled the search for efficient and sustainable renewable energy sources. Among these, solar photovoltaic technology stands out due to the abundance and cleanliness of sunlight. Within the photovoltaic landscape, thin film solar panels offer distinct advantages over traditional silicon-based modules, including reduced material usage, flexibility, and lower potential manufacturing costs. A leading contender in this field is the Copper Indium Gallium Selenide (CIGS)-based thin film solar panel, renowned for its high absorption coefficient, tunable bandgap, and exceptional long-term stability, achieving laboratory-scale conversion efficiencies exceeding 23%.
The heart of a CIGS thin film solar panel is its absorber layer, a polycrystalline semiconductor with the chemical formula CuIn(1-x)GaxSe2. The performance of the entire device is critically dependent on the composition, morphology, and crystalline quality of this layer. Consequently, developing low-cost, scalable, and high-quality deposition techniques for the CIGS absorber is paramount. While vacuum-based methods like co-evaporation and sputtering have yielded the highest efficiencies, they involve complex equipment and high energy consumption. Electrodeposition (ED) emerges as a highly promising non-vacuum, solution-based alternative. It offers significant advantages such as low-temperature processing, high material utilization, inherent scalability for large-area deposition, and relatively simple instrumentation. This article provides a comprehensive, first-person perspective on the research status, fundamental principles, challenges, and future trends of using electrodeposition to fabricate the absorber layer for CIGS thin film solar panels.
Fundamental Material Science of CIGS Absorbers
CIGS is a direct bandgap semiconductor derived from the parent compound CuInSe2 (CIS) by partially substituting indium with gallium. This alloying is the key to its success in thin film solar panels. The bandgap energy (Eg) of CIS is approximately 1.04 eV, which is lower than the ideal range for single-junction solar cells. By alloying with Ga to form CuIn(1-x)GaxSe2, the bandgap can be continuously tuned according to the relation:
$$E_g(x) \approx 1.04 + 0.67x – 0.17x(1-x) \text{ eV}$$
This allows for an optimal bandgap between 1.1 and 1.2 eV to be targeted, maximizing the match with the solar spectrum and thus the potential efficiency of the thin film solar panels. The material crystallizes in the chalcopyrite structure (space group I-42d), which is tolerant to a range of stoichiometries. However, high-efficiency devices typically require a slightly Cu-poor, (In+Ga)-rich overall composition. The [Ga]/([In]+[Ga]) ratio, or GGI, and the [Cu]/([In]+[Ga]) ratio, or CGI, are the two most critical compositional parameters governing the electronic properties and phase purity of the absorber layer in thin film solar panels.
Principles of Electrodeposition for CIGS
Electrodeposition is an electrochemical process where ions in a solution (electrolyte) are reduced at a conductive substrate (cathode) under an applied potential, forming a solid film. For multi-component systems like CIGS, the primary challenge is achieving simultaneous or sequential reduction of cations (Cu2+, In3+, Ga3+) and the anion precursor (often SeO32- or HSeO3+) to form a compound with the desired stoichiometry and phase.
The deposition process is governed by the Nernst equation for each species and the Butler-Volmer equation for kinetics. For a general reduction reaction: O + ne– ⇌ R, the current density (i) is given by:
$$i = i_0 \left[ \exp\left(\frac{\alpha_a F}{RT}(E-E_{eq})\right) – \exp\left(-\frac{\alpha_c F}{RT}(E-E_{eq})\right) \right]$$
where i0 is the exchange current density, α are charge transfer coefficients, F is Faraday’s constant, R is the gas constant, T is temperature, E is the applied potential, and Eeq is the equilibrium potential. The large differences in the standard reduction potentials of the constituent elements (e.g., Cu2+/Cu: ~0.34 V vs. SHE, In3+/In: -0.34 V vs. SHE, HSeO3+/Se: ~0.74 V vs. SHE) make co-deposition complex. This often necessitates the use of complexing agents to shift reduction potentials closer together or employing a non-aqueous medium with a wider electrochemical window.
The growth mechanism typically involves instantaneous nucleation and three-dimensional growth under diffusion control, described by models like the Scharifker-Hills theory. The morphology of the resulting film—whether it is compact, granular, or dendritic—profoundly affects the final performance of the thin film solar panels.
Electrodeposition from Aqueous Solutions
Aqueous electrodeposition has been the most extensively studied route due to the simplicity, low cost, and safety of water-based electrolytes. The approaches can be broadly classified into one-step co-deposition and multi-step (sequential) deposition.
One-Step Co-deposition
This method aims to deposit all four elements (Cu, In, Ga, Se) simultaneously from a single bath onto a conductive substrate, usually Molybdenum (Mo)-coated glass. The typical electrolyte contains soluble salts like CuSO4, In2(SO4)3, Ga2(SO4)3, and H2SeO3 or Na2SeO3. A supporting electrolyte (e.g., LiCl, KCl) is added for conductivity, and complexing agents like citric acid or tri-sodium citrate are crucial to bring the deposition potentials of In3+ and Ga3+ closer to that of Cu2+ and HSeO3+. The pH of the solution is a critical parameter, often maintained in the acidic range (2-3) to prevent hydroxide formation and stabilize the selenite species.
Despite its conceptual elegance, one-step aqueous co-deposition faces significant hurdles for thin film solar panels:
- Gallium Incorporation: Ga3+ has a very negative reduction potential and slow kinetics in aqueous media. Its incorporation is often insufficient and difficult to control, leading to a low GGI ratio in the as-deposited film, which limits the bandgap tunability.
- Hydrogen Evolution: The required negative deposition potential favors the competitive hydrogen evolution reaction (HER), especially on Mo. This can lead to porous, poorly adherent films with incorporated hydrogen defects.
- Stoichiometry Control: Achieving the precise Cu-poor, Group III-rich composition is challenging due to the different diffusion rates and reduction kinetics of the ions.
As-deposited films from one-step processes are typically amorphous or microcrystalline and consist of a mixture of binary and ternary phases (e.g., CuxSe, In2Se3, CuInSe2). A high-temperature annealing step (500-600°C) in a Se-containing atmosphere (selenization) is almost always mandatory to induce crystallization, promote grain growth, homogenize composition, and obtain the single-phase chalcopyrite CIGS required for high-efficiency thin film solar panels.
| Component | Typical Salt/Agent | Concentration Range (mM) | Primary Function |
|---|---|---|---|
| Copper Source | CuSO4·5H2O, CuCl2 | 1 – 10 | Provides Cu2+ ions |
| Indium Source | In2(SO4)3, InCl3 | 10 – 30 | Provides In3+ ions |
| Gallium Source | Ga2(SO4)3, GaCl3 | 5 – 20 | Provides Ga3+ ions |
| Selenium Source | H2SeO3, Na2SeO3 | 5 – 15 | Provides HSeO3+ / SeO32- |
| Complexing Agent | Citric Acid, Tri-sodium Citrate | 50 – 200 | Shifts In/Ga potentials, buffers pH |
| Supporting Electrolyte | LiCl, KCl, K2SO4 | 100 – 500 | Increases conductivity, mass transfer |
| pH Adjuster | HCl, H2SO4, KOH | To pH ~2.5 | Controls speciation and kinetics |
Multi-Step (Sequential) Deposition
To circumvent the limitations of co-deposition, sequential strategies were developed. A classic two-stage process involves first electrodepositing a metallic precursor stack (e.g., Cu/In/Ga or Cu-In-Ga alloy) followed by selenization. Another variant is the electrochemical deposition of a Cu-In-Ga-Se precursor with non-ideal stoichiometry, followed by additional electrodeposition of specific elements (e.g., more Cu or Se) to adjust the composition before the final thermal treatment. These methods offer better individual control over the deposition of each element, potentially improving film uniformity and adhesion. However, they add complexity to the process flow. The selenization step remains critical and must be carefully optimized to ensure complete reaction, uniform Ga distribution, and large grain growth, which are all vital for the performance of the resulting thin film solar panels.
Electrodeposition from Non-Aqueous Solutions
To overcome the fundamental limitations of aqueous systems—primarily the narrow electrochemical window and hydrogen evolution—research has expanded into non-aqueous solvents. These media allow the application of more negative potentials without solvent decomposition, facilitating the reduction of hard-to-deposit elements like Ga.
Organic Solvent-Based Systems
Polar aprotic organic solvents such as dimethyl sulfoxide (DMSO), dimethylformamide (DMF), and ethylene glycol have been investigated. These solvents can dissolve the necessary metal salts and offer wider potential windows (>3-4 V). For instance, ethanol-based baths have been used for one-step co-deposition, where the suppressed HER can lead to denser, more adherent precursor films. The chemistry of selenium reduction also differs in these media, sometimes leading to different intermediate phases. However, challenges include the lower conductivity of organic electrolytes (requiring supporting salts), potential moisture sensitivity, and the need for specialized handling and waste treatment, which can impact the cost-effectiveness goal for thin film solar panels.
Ionic Liquid-Based Systems
Room-temperature ionic liquids (RTILs) represent a revolutionary class of solvents for electrodeposition. They are composed entirely of ions, offering unique properties ideally suited for fabricating thin film solar panels:
- Wide Electrochemical Window: Often exceeding 5 V, enabling the deposition of very electronegative elements.
- Negligible Vapor Pressure: Non-flammable and allow for high-temperature processing without boiling.
- Good Ionic Conductivity: Facilitates electrochemical reactions.
- High Solubility for many metal salts.
Research has demonstrated the successful electrodeposition of In, Ga, Cu, and their alloys from various RTILs like 1-butyl-1-methylpyrrolidinium bis(trifluoromethylsulfonyl)imide ([BMP][Tf2N]) and 1-ethyl-3-methylimidazolium tetrafluoroborate ([EMIM][BF4]). More recently, one-step co-deposition of CIGS precursors has been achieved in ionic liquids or their mixtures with organic solvents (e.g., [BMIM][BF4] + ethanol). These precursors often exhibit better crystallinity and compositional uniformity in the as-deposited state. The absence of water eliminates hydrogen incorporation and oxide/hydroxide formation. While still in the exploratory stage, ionic liquid electrodeposition holds tremendous promise for producing high-quality CIGS absorbers for thin film solar panels with potentially fewer post-processing requirements, though the high cost and purification of RTILs are current barriers.
| Solvent System | Electrochemical Window | Key Advantages | Major Challenges | Typical Post-Deposition Treatment |
|---|---|---|---|---|
| Aqueous | ~1.23 V (theoretically, ~2 V practically) | Low cost, non-toxic, simple, scalable. | HER, limited Ga uptake, oxide formation. | Essential: High-T Selenization (≥550°C) |
| Organic (e.g., DMSO, Ethanol) | 3 – 4 V | Wider potential window, suppressed HER, denser films. | Lower conductivity, moisture sensitivity, cost. | Required: Annealing/Selenization |
| Ionic Liquid | > 4 – 5 V | Widest window, no HER, high-temperature stable, may yield crystalline as-deposited films. | High viscosity, high cost, purification, complex ion chemistry. | Potentially milder annealing possible. |
Key Challenges and Innovative Solutions
Despite decades of research, several persistent challenges must be addressed to elevate electrodeposited CIGS thin film solar panels to the efficiency and reliability levels of vacuum-based counterparts.
1. Precise Stoichiometry and Gallium Homogeneity: Controlling the GGI ratio uniformly through the film thickness is difficult. Ga tends to accumulate near the back contact (Mo) during selenization due to its lower diffusivity compared to In. Innovative approaches include:
- Pulse and Pulse-Reverse Electrodeposition: Applying tailored potential/current waveforms can improve nucleation density and composition control by modulating mass transport and surface reactions.
- Electrolyte Engineering: Using novel complexing agents or ionic liquid mixtures to tailor the reduction kinetics of Ga3+ specifically.
- Stacked Precursor Design: Engineering the sequence and thickness of individually deposited Cu, In, and Ga layers to create a desired compositional gradient after selenization.
2. Film Adhesion and Morphology: Poorly adherent, porous, or rough films lead to shunts and high series resistance in the final thin film solar panels. Solutions focus on:
- Substrate Modification: Engineering the Mo back contact morphology (e.g., creating a rough or textured surface) to enhance mechanical interlocking.
- Additives: Incorporating small amounts of grain refiners or surfactants (e.g., thiourea derivatives) in the electrolyte to promote smooth, compact growth.
- In-situ/Ex-situ Annealing: Developing rapid thermal processing (RTP) or laser annealing to quickly recrystallize the film without delamination.
3. Post-Deposition Selenization: This high-temperature step (often involving toxic H2Se or Se vapor) is a bottleneck. Research aims at:
- Reactive Annealing: Using elemental Se vapor in a controlled atmosphere rather than H2Se.
- Solid-State Selenization: Employing Se-containing layers (e.g., evaporated Se) in contact with the precursor film.
- Low-Temperature Crystallization: Exploring pathways in ionic liquids or using photonic curing to induce crystallization at temperatures compatible with flexible polymer substrates, a key advantage for next-generation lightweight thin film solar panels.
4. Efficiency Limitations: The best reported efficiencies for fully electrodeposited CIGS thin film solar panels remain around 15-16%, lagging behind the >23% of vacuum methods. The primary culprits are believed to be:
- High defect densities (especially at grain boundaries) leading to recombination.
- Non-optimal bandgap grading due to Ga inhomogeneity.
- Interface issues with the CdS buffer layer.
Intensive research is focused on understanding and passivating these defects through post-deposition treatments (e.g., Alkali post-deposition treatment with NaF or KF), which is also crucial for electrodeposited absorbers.
Integration and Scale-Up: From Lab to Module
The true test for any deposition technology is its scalability and integration into a full device and module manufacturing line. For electrodeposition in thin film solar panels, this involves:
- Continuous Processing: Developing roll-to-roll (R2R) or sheet-to-sheet electrodeposition systems for flexible substrates (metal foils, polyimide). This is a major advantage of solution processing.
- Monolithic Interconnection: Patterning the Mo back contact and the absorber layer itself to create series-connected cells on a single substrate, a standard practice in thin film solar panel module fabrication. Electrodeposition can be adapted for this through laser scribing or patterned masking.
- Process Compatibility: Ensuring the electrodeposited and annealed CIGS film provides a suitable surface for the subsequent chemical bath deposition (CBD) of the CdS buffer layer and the sputtering of the transparent conductive oxide (TCO) front contact.
- Environmental and Cost Analysis: A full life-cycle assessment (LCA) is necessary to validate the environmental and economic benefits of the electrodeposition route, considering all chemicals, energy use for annealing, and waste streams.
Future Trends and Perspectives
The future of electrodeposition for CIGS thin film solar panels is vibrant and points towards hybrid and intelligent processes.
1. Hybrid Deposition Strategies: Combining electrodeposition with other techniques will likely yield the best results. For example:
- Electrodepositing a precise Cu-In-Ga metallic precursor followed by rapid thermal selenization using a physical vapor deposition (PVD) Se source.
- Using electrodeposition to form a thin, dense seed layer, followed by a faster growth step like nanoparticle printing or electroless deposition.
2. Advanced Electrolyte Design: The exploration of deep eutectic solvents (DES) as cheaper, tunable alternatives to ionic liquids. Machine learning could be employed to screen vast combinations of ions, complexing agents, and additives to design optimal electrolytes for specific film properties.
3. Beyond Selenization – Sulfur and Alloying: Research is expanding into Cu(In,Ga)(S,Se)2 (CIGSSe) alloys, where sulfur incorporation can widen the bandgap further and improve VOC. Electrodeposition from baths containing both Se and S precursors is an emerging area.
4. In-situ Diagnostics and Control: Implementing real-time monitoring techniques like electrochemical quartz crystal microbalance (EQCM), spectroscopic ellipsometry, or potential/current noise analysis to gain feedback and control over the growth process, moving towards a fully controlled, reproducible manufacturing process for thin film solar panels.
5. Alternative Architectures: Electrodeposition could be ideal for fabricating nanostructured CIGS absorbers (e.g., nanowires, nano-columns) using templated substrates, which could offer novel light-trapping and carrier collection benefits for next-generation thin film solar panels.
| Focus Area | Current Status/Challenge | Future Direction | Potential Impact |
|---|---|---|---|
| Stoichiometry Control | Difficult Ga incorporation and homogeneity. | AI-driven electrolyte design; Pulsed electrodeposition with real-time feedback. | Precise bandgap grading, higher VOC and efficiency. |
| Post-Deposition Annealing | High-temperature selenization bottleneck. | Photonic/Plasma/Laser curing; Low-temperature ionic liquid processing. | Enable flexible substrates, lower energy cost, faster processing. |
| Film Morphology | Porosity and adhesion issues. | Nanoparticle-assisted electrodeposition; Advanced substrate engineering. | Dense, large-grained films, reduced recombination. |
| Process Integration | Lab-scale demonstrations. | Development of R2R electrodeposition lines; Hybrid ED/PVD processes. | Scalable, low-cost manufacturing of large-area thin film solar panels. |
| Material System | Primarily CIGS. | Exploration of CIGSSe, CZTSSe (kesterites) via electrodeposition. | Abundant, non-toxic alternatives, broader application space. |
In conclusion, electrodeposition remains a highly promising and dynamic pathway for fabricating the absorber layer of CIGS thin film solar panels. Its inherent advantages in cost, scalability, and material efficiency align perfectly with the goals of terawatt-scale photovoltaics. While challenges in compositional control, post-processing, and ultimate efficiency persist, ongoing research in non-aqueous chemistry, hybrid processes, and advanced engineering is steadily addressing these limitations. The future likely belongs not to a single deposition method, but to intelligent, integrated manufacturing flows where electrodeposition plays a critical role in enabling low-cost, high-performance, and potentially flexible thin film solar panels for a wide array of applications.