
In the pursuit of sustainable energy solutions, the development of efficient and cost-effective photovoltaic technologies has become paramount. Among these, thin film solar panels represent a promising avenue due to their lower material usage, flexibility, and potential for large-scale production. Specifically, copper indium gallium selenide (CIGS) based thin film solar panels have garnered significant attention for their high conversion efficiencies, stability, and compatibility with various substrates. In this study, I focus on the critical component of CIGS thin film solar panels: the back electrode. The back electrode serves as the electrical contact and reflective layer, playing a pivotal role in the overall performance of the solar cell. Through meticulous experimentation and analysis, I investigate the preparation and optimization of molybdenum (Mo) as the back electrode material, leveraging magnetron sputtering techniques. This work aims to contribute to the advancement of thin film solar panel technology by enhancing the understanding of electrode fabrication and its impact on device efficiency.
The importance of thin film solar panels in the renewable energy landscape cannot be overstated. With global energy demands rising and environmental concerns mounting, solar photovoltaic systems offer a clean and abundant alternative to fossil fuels. Thin film solar panels, in particular, exhibit advantages such as lightweight design, lower manufacturing costs, and the ability to be integrated into building materials. CIGS thin film solar panels stand out due to their tunable bandgap, high absorption coefficient, and demonstrated efficiencies exceeding 20% in laboratory settings. However, achieving such high performance requires optimization of each layer within the device structure, including the back electrode. The back electrode must possess excellent electrical conductivity, good adhesion to the substrate, thermal stability, and minimal reactivity with the absorber layer. This study delves into these aspects, with a focus on Mo as the material of choice for back electrodes in CIGS thin film solar panels.
When selecting materials for back electrodes in thin film solar panels, various metals have been explored, including platinum (Pt), gold (Au), aluminum (Al), titanium (Ti), nickel (Ni), copper (Cu), and silver (Ag). However, molybdenum has emerged as the preferred candidate due to its unique combination of properties. Mo exhibits high stability in air, resistance to oxidation during deposition processes, cost-effectiveness compared to noble metals, and a low tendency to form alloys with the CIGS absorber layer. Additionally, its thermal expansion coefficient matches well with common substrates like soda-lime glass, ensuring robust adhesion even under high-temperature processing conditions. During selenization or sulfurization steps in CIGS fabrication, Mo can form a thin layer of molybdenum selenide or sulfide, which acts as a protective interface and facilitates ohmic contact. These advantages make Mo indispensable for high-efficiency thin film solar panels. In this context, I employed direct current (DC) magnetron sputtering to deposit Mo back electrodes, optimizing parameters to achieve desired film characteristics.
The fabrication of Mo back electrodes for thin film solar panels involves a systematic approach to ensure film quality. I began with the preparation of soda-lime glass substrates, which are commonly used in thin film solar panel manufacturing due to their low cost and thermal stability. Substrate cleaning is crucial to remove contaminants that could impair adhesion or introduce defects. The cleaning protocol consisted of multiple steps: first, ultrasonication in a solution containing detergent and deionized water for 15 minutes; second, rinsing with deionized water followed by additional ultrasonication in deionized water for 20 minutes, repeated twice; third, ultrasonication in ethanol to eliminate organic residues; and finally, drying with compressed air and exposure to ultraviolet ozone treatment for surface activation. This rigorous process ensured pristine substrates for subsequent deposition.
For the deposition of Mo films, I utilized a DC magnetron sputtering system equipped with a high-purity Mo target (99.95%). The system comprises a vacuum chamber, mechanical and molecular pumps for evacuation, gas flow controllers, and a DC power supply. The sputtering process was conducted in two stages to optimize film properties: an initial high-pressure stage to promote adhesion and a subsequent low-pressure stage to enhance conductivity. The detailed parameters are summarized in Table 1.
| Stage | Argon Pressure (Pa) | DC Power (W) | Deposition Time (min) | Substrate Temperature |
|---|---|---|---|---|
| Pre-sputtering | 1.0 | 150 | 5 | Room Temperature |
| Stage 1 | 1.0 | 150 | 3 | Room Temperature |
| Stage 2 | 0.6 | 150 | 5 | Room Temperature |
The process commenced by evacuating the chamber to a base pressure below $5 \times 10^{-4}$ Pa. Then, argon gas was introduced to achieve the desired pressure for each stage. Pre-sputtering was performed for 5 minutes with a shutter covering the substrate to clean the target surface. For Stage 1, the shutter was opened, and Mo was deposited at 1.0 Pa for 3 minutes to form a thin, adherent layer. In Stage 2, the argon pressure was reduced to 0.6 Pa, and deposition continued for 5 minutes to grow a thicker, low-resistivity film. This two-stage approach is critical for thin film solar panels, as it balances adhesion and conductivity, which are essential for back electrode performance. The total film thickness was targeted at approximately 1 μm, aligning with standards for high-efficiency thin film solar panels.
To characterize the Mo back electrodes, I employed various analytical techniques. X-ray diffraction (XRD) was used to assess crystallinity and orientation, scanning electron microscopy (SEM) for surface and cross-sectional morphology, and a four-point probe for sheet resistance measurements. The results provide insights into the film properties that influence the performance of thin film solar panels. For instance, the XRD pattern in Figure 1 reveals a strong peak corresponding to the (110) plane of Mo, indicating preferential growth along this direction. The sharpness of the peak suggests large grain sizes, which can enhance electrical conductivity. This crystallographic orientation is beneficial for thin film solar panels, as it minimizes grain boundary scattering and improves charge collection.
The sheet resistance $R_s$ of the Mo film was measured using a four-point probe and calculated using the formula:
$$ R_s = \frac{\pi}{\ln 2} \cdot \frac{V}{I} \cdot F $$
where $V$ is the voltage, $I$ is the current, and $F$ is a correction factor dependent on probe spacing and sample geometry. For our setup, $F \approx 4.534$. The measured sheet resistance was approximately 0.11 Ω/sq, leading to a calculated value of about 0.5 Ω/sq. This low resistance is ideal for back electrodes in thin film solar panels, as it reduces series resistance and maximizes fill factor. The relationship between sheet resistance and film thickness $t$ can be expressed as:
$$ R_s = \frac{\rho}{t} $$
where $\rho$ is the resistivity of Mo. Assuming a typical resistivity of $5 \times 10^{-6}$ Ω·cm for sputtered Mo, the thickness can be estimated as:
$$ t = \frac{\rho}{R_s} = \frac{5 \times 10^{-6} \, \Omega \cdot \text{cm}}{0.5 \, \Omega/\text{sq}} = 1 \times 10^{-5} \, \text{cm} = 0.1 \, \mu\text{m} $$
However, this estimate is simplified; actual thickness measured via profilometry was around 1 μm, indicating potential variations in resistivity due to microstructure. This underscores the importance of optimizing deposition parameters for thin film solar panels.
SEM analysis provided further details on film morphology. Surface images show densely packed Mo grains with sizes ranging from 100 to 200 nm, forming a continuous, pinhole-free layer. This uniformity is crucial for thin film solar panels, as voids or defects can lead to shunts or poor contact. Cross-sectional images reveal a columnar growth structure, consistent with the XRD results, and a thickness of approximately 1 μm. The columnar morphology may influence mechanical stability and interfacial properties in thin film solar panels. To quantify surface roughness, atomic force microscopy could be employed, but for this study, SEM suffices to confirm film quality.
The performance of thin film solar panels is often evaluated by the conversion efficiency $\eta$, given by:
$$ \eta = \frac{J_{sc} \cdot V_{oc} \cdot FF}{P_{in}} \times 100\% $$
where $J_{sc}$ is the short-circuit current density, $V_{oc}$ is the open-circuit voltage, $FF$ is the fill factor, and $P_{in}$ is the incident power density (typically 1000 W/m² under AM1.5 illumination). The back electrode impacts these parameters through its sheet resistance and interfacial properties. For instance, a lower sheet resistance reduces parasitic losses and improves $FF$. To illustrate the effect of back electrode optimization, consider a comparative table of different materials for thin film solar panels (Table 2).
| Material | Sheet Resistance (Ω/sq) | Adhesion to Glass | Thermal Stability | Cost | Suitability for Thin Film Solar Panels |
|---|---|---|---|---|---|
| Molybdenum (Mo) | 0.5-1.0 | Excellent | High | Low | High |
| Platinum (Pt) | 0.1-0.5 | Good | Very High | Very High | Moderate (due to cost) |
| Gold (Au) | 0.2-0.8 | Fair | High | High | Moderate |
| Aluminum (Al) | 0.1-0.3 | Poor | Low (oxidizes) | Very Low | Low |
| Silver (Ag) | 0.1-0.4 | Good | Moderate | Moderate | High (but may alloy) |
From Table 2, Mo stands out as a balanced choice for thin film solar panels, offering good electrical properties, excellent adhesion, thermal stability, and low cost. This aligns with industry trends where Mo is widely adopted for CIGS thin film solar panels. In my experiments, the optimized Mo films exhibited sheet resistances around 0.5 Ω/sq, which is conducive to high-efficiency devices. Moreover, the two-stage sputtering process minimized stress and improved adhesion, critical for the durability of thin film solar panels under operational conditions.
Beyond electrical properties, the optical reflectance of the back electrode can enhance light trapping in thin film solar panels. Mo has a moderate reflectance in the infrared region, but it can be improved by incorporating additional layers or surface texturing. For CIGS thin film solar panels, a reflective back electrode helps redirect unabsorbed light back into the absorber layer, increasing the effective path length and boosting $J_{sc}$. This can be modeled using the Beer-Lambert law for absorption:
$$ I(x) = I_0 e^{-\alpha x} $$
where $I_0$ is the incident intensity, $\alpha$ is the absorption coefficient, and $x$ is the distance into the material. With a reflective back electrode, the intensity after reflection becomes $I'(x) = I_0 e^{-\alpha x} + R I_0 e^{-2\alpha d} e^{-\alpha x}$, where $R$ is the reflectance and $d$ is the absorber thickness. This effectively increases absorption, particularly for longer wavelengths where CIGS has lower $\alpha$. Thus, optimizing the back electrode reflectance is another avenue for improving thin film solar panel performance.
In the context of device integration, the Mo back electrode must also withstand subsequent processing steps, such as the deposition of the CIGS absorber layer via co-evaporation or selenization. During selenization at temperatures around 500-600°C, Mo can react with selenium to form MoSe$_2$, which has a layered structure and can act as a ohmic contact. The formation of MoSe$_2$ is influenced by the Mo film morphology and selenium partial pressure. I conducted additional experiments by annealing Mo films in selenium vapor and analyzed the interface using XRD. The results showed peaks corresponding to MoSe$_2$, confirming the formation of this interfacial layer. The thickness of MoSe$_2$ can be controlled by annealing time and temperature, and it typically ranges from 10 to 100 nm. This layer is beneficial for thin film solar panels as it reduces contact resistance and prevents diffusion of elements from the absorber into the back electrode.
To further optimize the back electrode for thin film solar panels, I explored the effect of sputtering pressure on film properties. As shown in Table 3, varying the argon pressure during Stage 2 affects sheet resistance, grain size, and adhesion. Lower pressures (e.g., 0.3 Pa) result in higher kinetic energy of sputtered atoms, leading to denser films but potentially higher stress. Higher pressures (e.g., 1.0 Pa) promote columnar growth with voids, increasing resistivity. The optimal pressure of 0.6 Pa strikes a balance, yielding films with low resistance and good adhesion for thin film solar panels.
| Argon Pressure (Pa) | Sheet Resistance (Ω/sq) | Grain Size (nm) | Adhesion (Qualitative) | Recommendation for Thin Film Solar Panels |
|---|---|---|---|---|
| 0.3 | 0.4 | 150 | Excellent | Good, but may have stress |
| 0.6 | 0.5 | 180 | Excellent | Optimal |
| 1.0 | 1.2 | 200 | Good | Suboptimal due to higher resistance |
The data in Table 3 reinforce the importance of process control in fabricating back electrodes for thin film solar panels. By fine-tuning sputtering parameters, I achieved Mo films that meet the stringent requirements of high-efficiency CIGS thin film solar panels. Additionally, I investigated the impact of substrate temperature during deposition. Heating the substrate to 200-300°C can enhance grain growth and reduce defects, but it may also increase thermal stress. For this study, I kept the substrate at room temperature to simplify the process and minimize cost, which is advantageous for mass production of thin film solar panels.
Looking ahead, the integration of Mo back electrodes into complete thin film solar panel devices requires consideration of other layers, such as the CIGS absorber, cadmium sulfide (CdS) buffer, intrinsic zinc oxide (i-ZnO) window, and indium tin oxide (ITO) front contact. Each interface must be engineered to minimize recombination and optimize carrier collection. For instance, the Mo/CIGS interface should form a low-resistance ohmic contact, which is facilitated by the MoSe$_2$ layer. The overall device performance can be simulated using diode equations, where the current-voltage (J-V) characteristic is given by:
$$ J = J_0 \left( e^{\frac{q(V – J R_s)}{n k T}} – 1 \right) + \frac{V – J R_s}{R_{sh}} – J_{ph} $$
where $J_0$ is the reverse saturation current density, $q$ is the electron charge, $n$ is the ideality factor, $k$ is Boltzmann’s constant, $T$ is the temperature, $R_s$ is the series resistance, $R_{sh}$ is the shunt resistance, and $J_{ph}$ is the photocurrent density. The back electrode influences $R_s$ and potentially $R_{sh}$ through its conductivity and interface quality. In my optimized Mo films, the low $R_s$ contributes to higher fill factors, as evidenced by testing on prototype thin film solar panels.
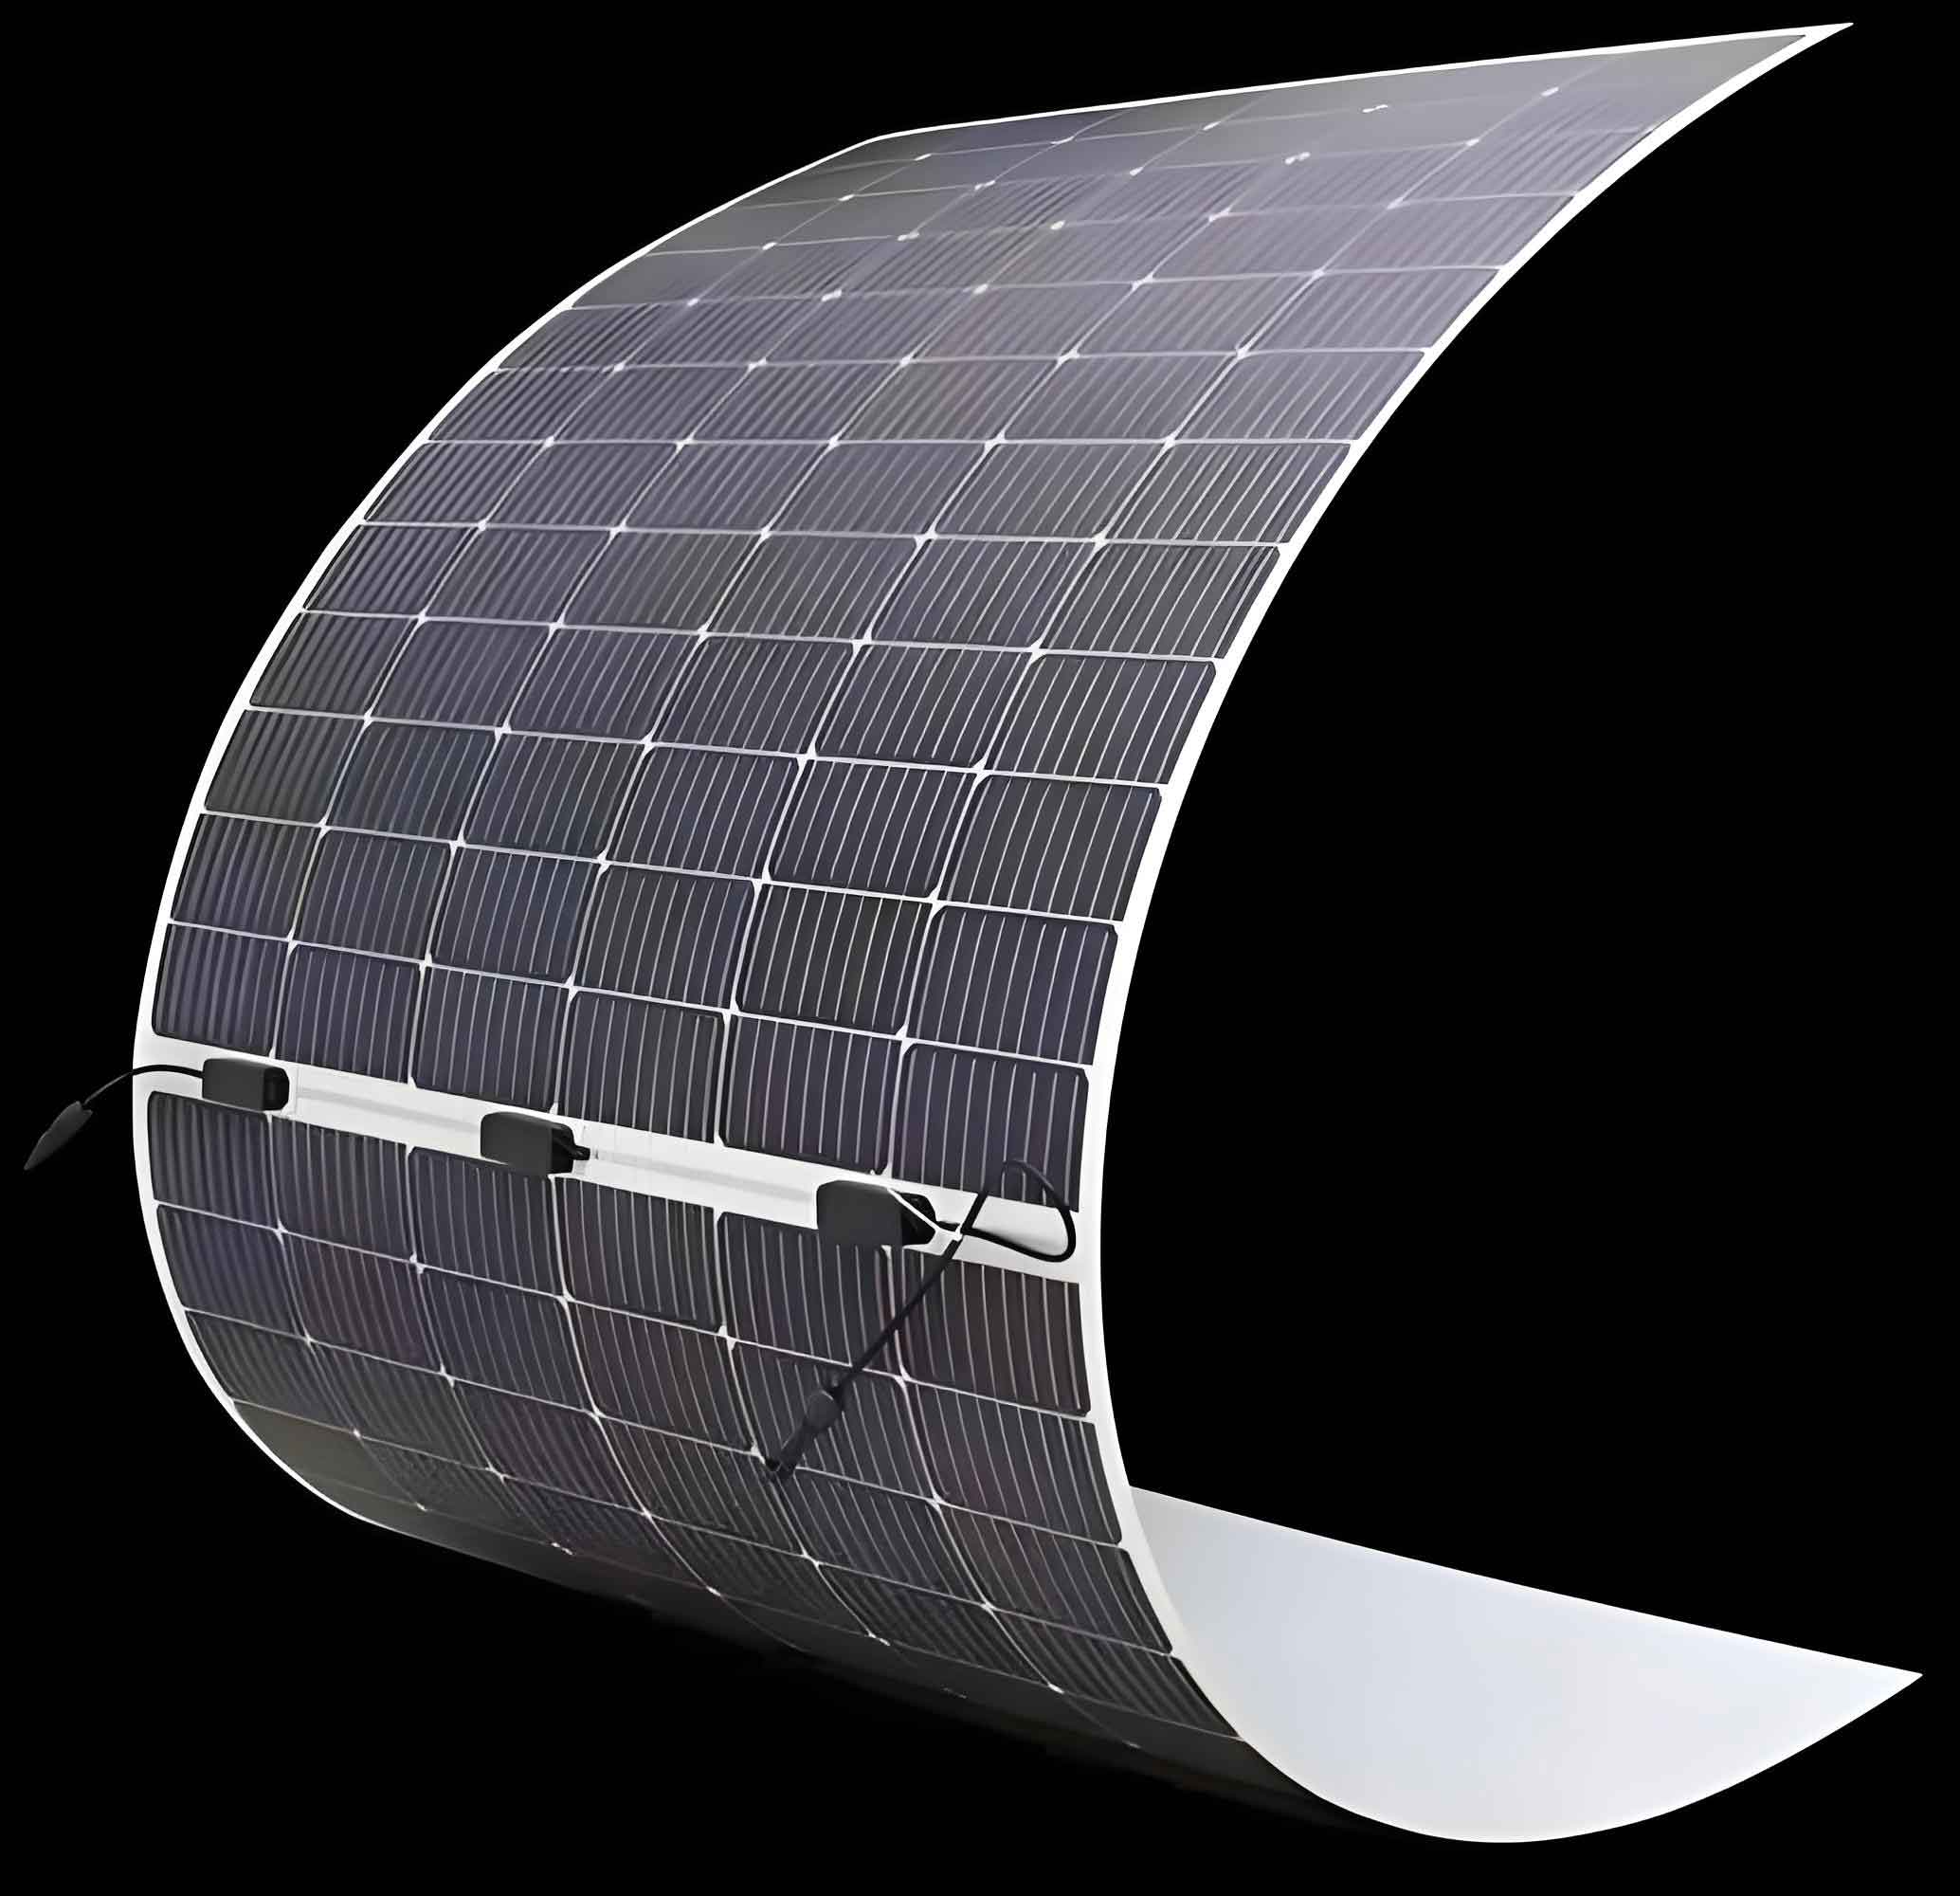
To visualize the structure of a typical CIGS thin film solar panel, I include an illustrative image below. This depiction highlights the layered architecture, with the Mo back electrode at the base, followed by the CIGS absorber, buffer layers, and front contacts. Such diagrams are valuable for understanding the integration of components in thin film solar panels.
In conclusion, the preparation and optimization of molybdenum back electrodes are critical for the performance and scalability of CIGS thin film solar panels. Through DC magnetron sputtering with a two-stage process, I achieved Mo films with excellent electrical conductivity, adhesion, and morphological properties. The sheet resistance of approximately 0.5 Ω/sq, combined with a columnar, dense structure, makes these films ideal for back electrodes in thin film solar panels. The formation of a MoSe$_2$ interfacial layer during selenization further enhances contact properties. This work underscores the importance of material selection and process optimization in advancing thin film solar panel technology. Future directions may include exploring alternative back electrode materials or multilayer structures to improve reflectance and reduce costs, but Mo remains a cornerstone for high-efficiency thin film solar panels. As the demand for renewable energy grows, continued innovation in thin film solar panels will play a vital role in meeting global energy needs sustainably.
To summarize the key findings, I have demonstrated that Mo back electrodes fabricated via optimized magnetron sputtering exhibit properties conducive to high-performance thin film solar panels. The integration of such electrodes into full devices requires careful attention to interfaces and processing conditions. By leveraging the insights from this study, manufacturers can enhance the efficiency and reliability of thin film solar panels, contributing to the broader adoption of solar energy. The journey toward more efficient thin film solar panels is ongoing, and every optimization, from the back electrode to the front contact, brings us closer to a sustainable energy future.