
In the context of the global energy transition, the development of efficient energy storage technology is paramount. Among the various options, the lithium-ion battery stands out due to its high energy density, excellent power capability, long cycle life, and relatively low cost, making it a cornerstone for modern portable electronics, electric vehicles, and grid storage solutions. The performance, safety, and longevity of a lithium-ion battery are fundamentally determined by the quality of its electrodes. The electrode manufacturing process involves several critical steps, with the drying of the wet slurry coating being one of the most energy-intensive and quality-defining stages.
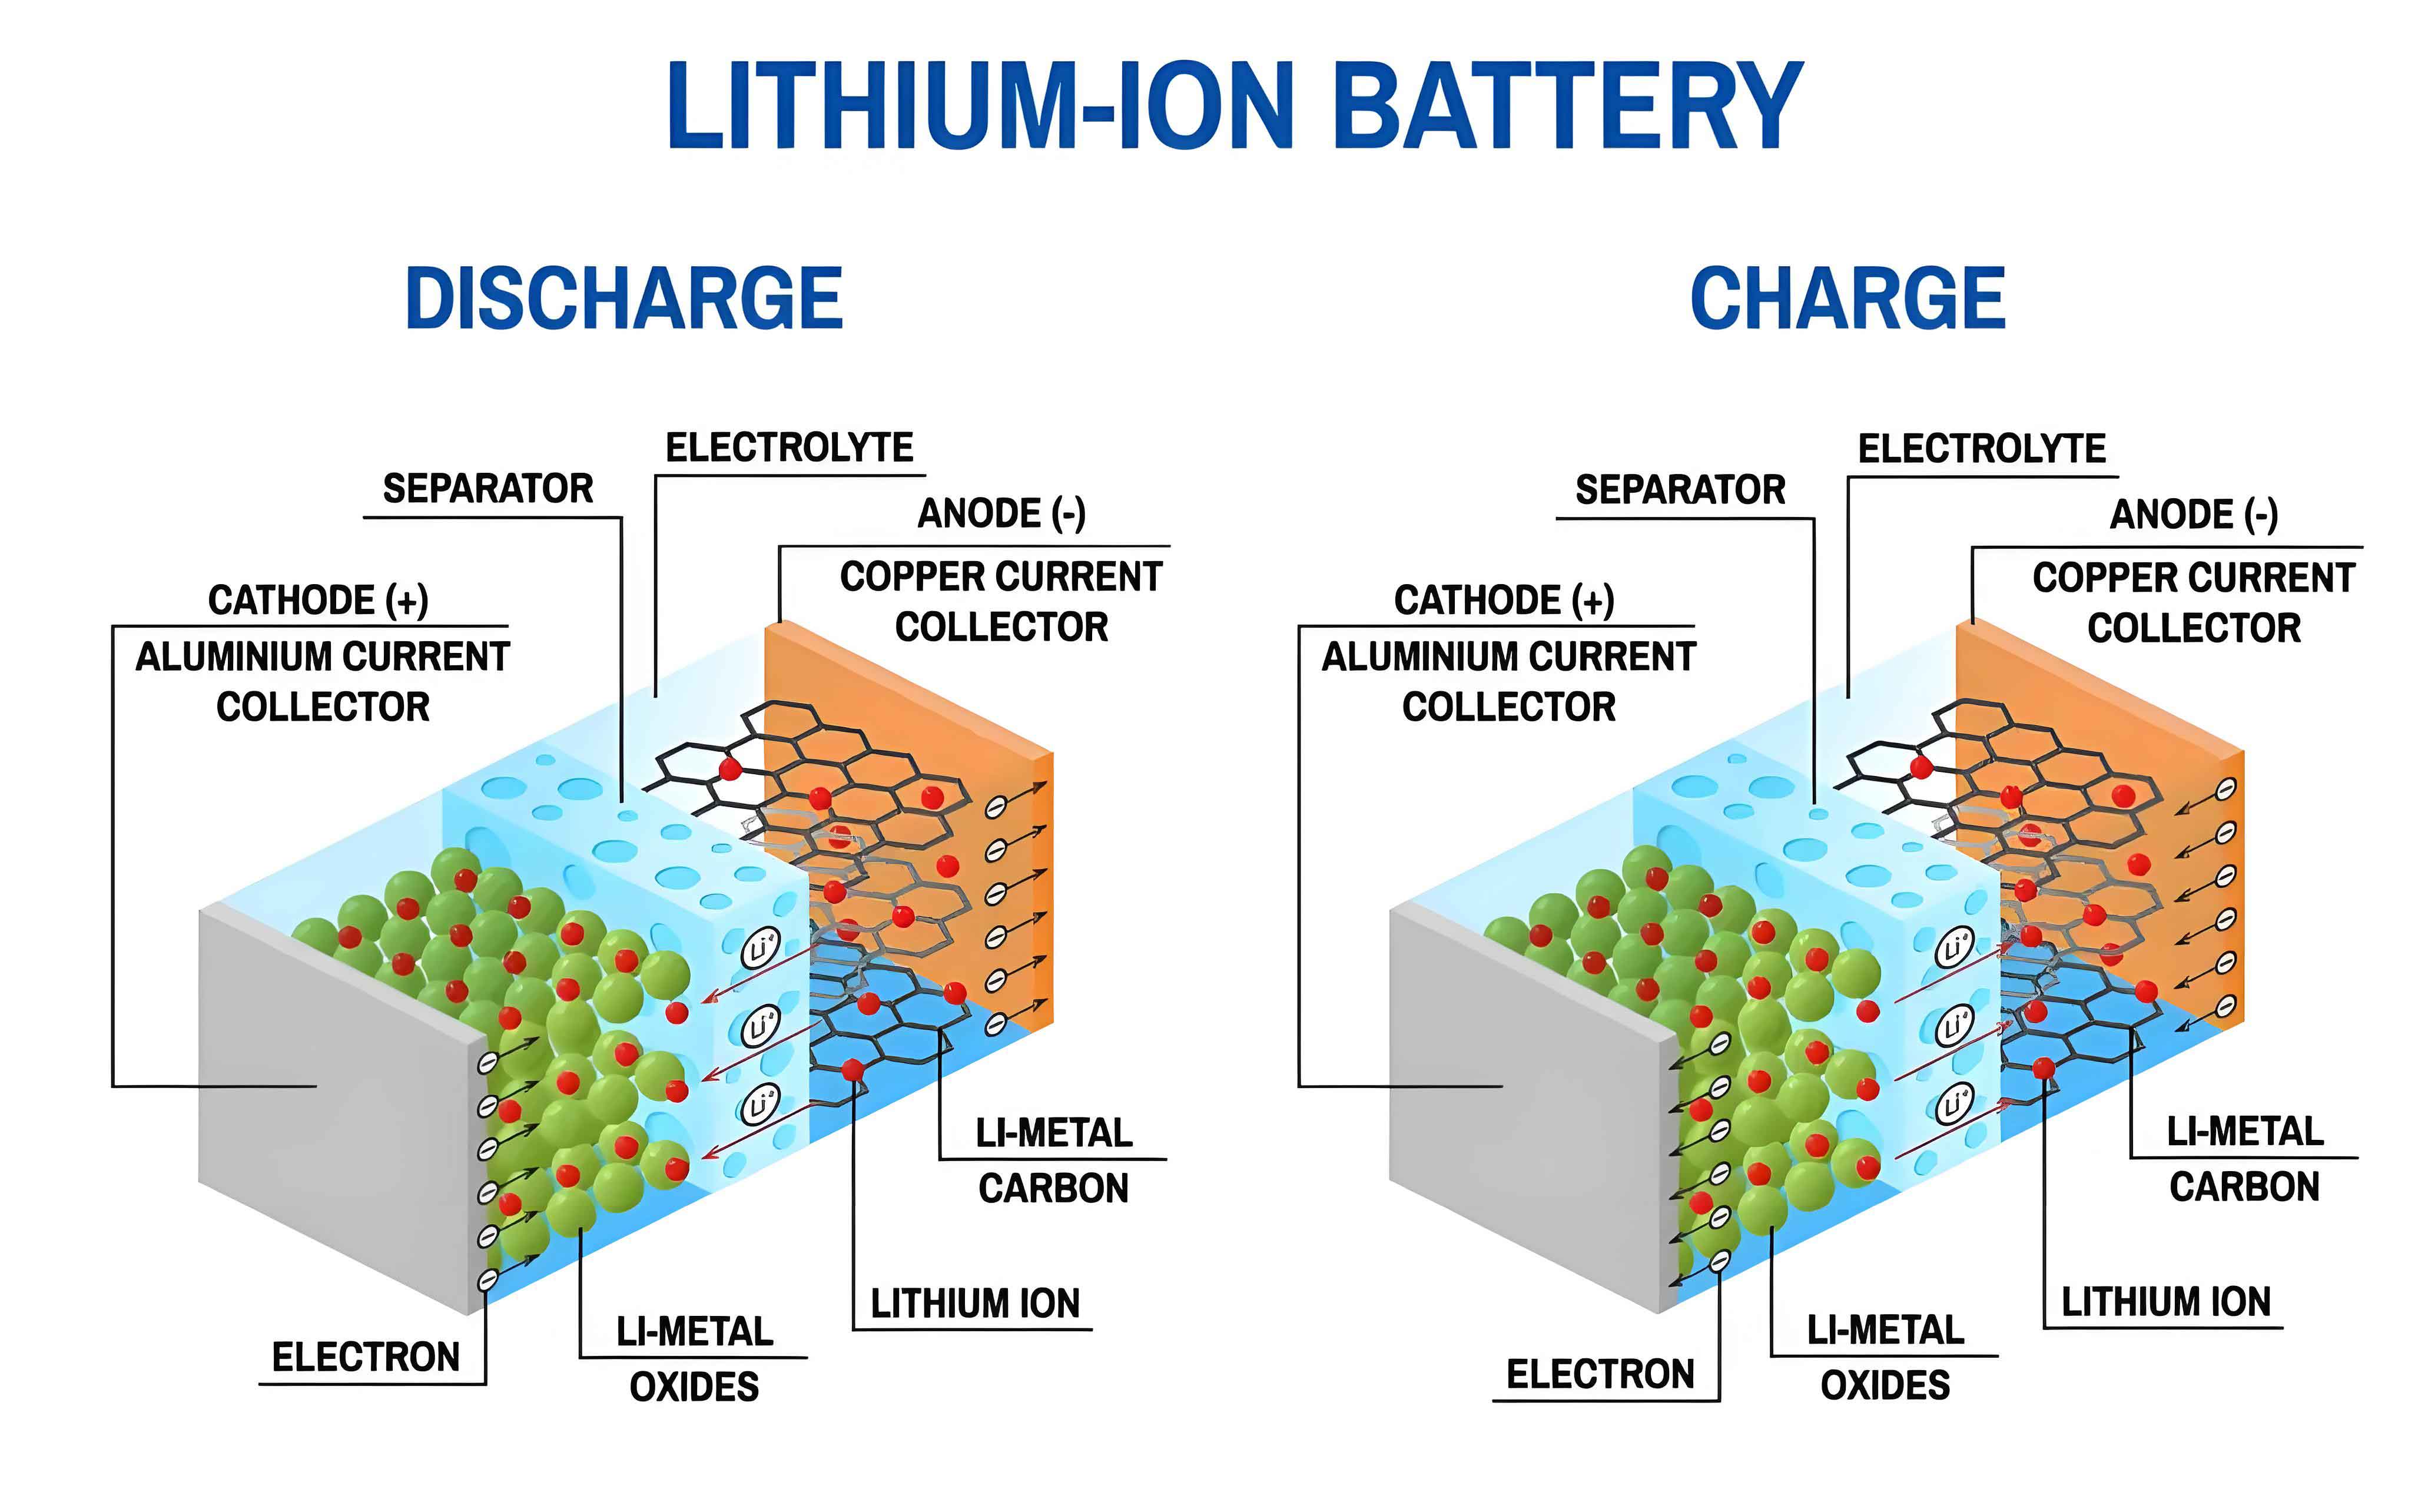
During drying, the solvent (e.g., N-Methyl-2-pyrrolidone for cathodes) must be removed uniformly from the porous composite structure comprising active material particles, conductive carbon, and polymeric binder. An overly rapid drying rate can lead to binder migration, causing a non-uniform distribution that compromises adhesion and electronic conductivity, or result in crack formation within the coating. Conversely, excessively slow drying is inefficient, increases production costs and energy consumption, and may leave residual solvent that can degrade lithium-ion battery performance during operation. Therefore, gaining a deep understanding of the drying mechanisms and the influence of process parameters is essential for optimizing this step in lithium-ion battery manufacturing.
However, the drying process involves complex, coupled phenomena of multiphase flow, heat transfer, and mass transfer within a porous medium. It is exceedingly difficult to obtain detailed, real-time data on internal moisture distribution, temperature gradients, and evaporation rates through industrial trials or conventional physical experiments alone. This lack of visibility into the “process black box” hinders fundamental analysis and targeted optimization. Computational Fluid Dynamics (CFD) has emerged as a powerful tool to overcome these limitations. By constructing accurate numerical models, CFD allows for the virtual exploration of drying dynamics under various conditions at a fraction of the cost and time required for physical experimentation. This study employs a CFD-based approach to develop a coupled model of a suspension drying air field and the lithium-ion battery electrode itself. The primary objective is to systematically investigate the impact of key operational parameters—specifically, the time-varying profile of the drying air temperature and the inlet air velocity—on the drying rate and associated energy consumption, thereby providing a theoretical foundation for process optimization.
1. Governing Equations and Model Development
The modeling framework consists of two interlinked components: a steady-state model for the air flow in the suspension drying nozzle system, and a transient model for the solvent evaporation within the porous electrode coating. A one-way coupling is assumed, where the air field dictates the boundary conditions (heat and mass transfer coefficients) for the electrode model, while the influence of the thin electrode’s evaporation on the bulk air flow is considered negligible.
1.1 Suspension Drying Air Field Model
The steady-state airflow is governed by the Reynolds-Averaged Navier-Stokes (RANS) equations. For an incompressible flow, the continuity and momentum equations are given by:
$$
\frac{\partial \bar{u}_j}{\partial x_j} = 0
$$
$$
\rho_a \bar{u}_j \frac{\partial \bar{u}_i}{\partial x_j} = -\frac{\partial \bar{p}}{\partial x_i} + \frac{\partial}{\partial x_j}\left[ \mu_a \left( \frac{\partial \bar{u}_i}{\partial x_j} + \frac{\partial \bar{u}_j}{\partial x_i} \right) – \rho_a \overline{u_i’ u_j’} \right]
$$
where $\bar{u}_i$ are the mean velocity components, $\bar{p}$ is the mean pressure, $\rho_a$ is the air density, and $\mu_a$ is the dynamic viscosity. The term $\rho_a \overline{u_i’ u_j’}$ represents the Reynolds stresses, which must be modeled to close the system of equations.
The energy equation for temperature transport is:
$$
\rho_a c_{p,a} \bar{u}_j \frac{\partial T}{\partial x_j} = \frac{\partial}{\partial x_j} \left( \frac{\mu_a}{Pr} \frac{\partial T}{\partial x_j} – \rho_a c_{p,a} \overline{T’ u_j’} \right)
$$
where $T$ is the temperature, $c_{p,a}$ is the specific heat capacity of air, $Pr$ is the Prandtl number, and $\overline{T’ u_j’}$ is the turbulent heat flux.
To model the turbulence, the Shear Stress Transport (SST) $k-\omega$ model is employed due to its accurate performance in predicting flows with adverse pressure gradients and separation, which are common in impingement-type drying. The transport equations for turbulent kinetic energy $k$ and specific dissipation rate $\omega$ are:
$$
\frac{\partial}{\partial x_j} (\rho_a k \bar{u}_j) = \frac{\partial}{\partial x_j} \left( \Gamma_k \frac{\partial k}{\partial x_j} \right) + G_k – Y_k + S_k
$$
$$
\frac{\partial}{\partial x_j} (\rho_a \omega \bar{u}_j) = \frac{\partial}{\partial x_j} \left( \Gamma_{\omega} \frac{\partial \omega}{\partial x_j} \right) + G_{\omega} – Y_{\omega} + D_{\omega} + S_{\omega}
$$
Here, $\Gamma_k$ and $\Gamma_{\omega}$ are the effective diffusivities, $G_k$ and $G_{\omega}$ are the generation terms, $Y_k$ and $Y_{\omega}$ are the dissipation terms, $D_{\omega}$ is the cross-diffusion term, and $S_k$, $S_{\omega}$ are user-defined source terms.
1.2 Solvent Evaporation Model in the Porous Electrode
The wet electrode coating is treated as a capillary porous medium undergoing a drying process. The model tracks the transport of liquid solvent, solvent vapor, and air within the pores, coupled with heat transfer. The governing equations are based on conservation of mass for each phase and conservation of energy.
Mass Conservation for Liquid Solvent:
$$
\frac{\partial}{\partial t} (\rho_l \varepsilon S_l) + \frac{\partial}{\partial z} (n_l) = -\dot{m}
$$
Mass Conservation for Solvent Vapor:
$$
\frac{\partial}{\partial t} (\rho_v \varepsilon S_g) + \frac{\partial}{\partial z} (n_v) = \dot{m}
$$
Mass Conservation for Air:
$$
\frac{\partial}{\partial t} (\rho_a \varepsilon S_g) + \frac{\partial}{\partial z} (n_a) = 0
$$
Energy Conservation:
$$
(\rho c_p)_{\text{eff}} \frac{\partial T}{\partial t} = \frac{\partial}{\partial z} \left( \lambda_{\text{eff}} \frac{\partial T}{\partial z} \right) – h_{\text{vap}} \dot{m}
$$
In these equations:
- $\varepsilon$ is the porosity of the coating.
- $S_l$ and $S_g$ are the saturations of liquid and gas phases, with $S_l + S_g = 1$.
- $\rho_l$, $\rho_v$, $\rho_a$ are the densities of liquid solvent, solvent vapor, and air, respectively.
- $n_l$, $n_v$, $n_a$ are the flux of liquid, vapor, and air. Liquid flux is driven by capillary pressure gradients (Darcy’s law), while vapor and air fluxes are driven by diffusion and pressure gradients.
- $\dot{m}$ is the volumetric evaporation rate, typically calculated based on the difference between the vapor pressure at the liquid interface and the partial pressure in the gas phase.
- $h_{\text{vap}}$ is the latent heat of vaporization.
- $(\rho c_p)_{\text{eff}}$ and $\lambda_{\text{eff}}$ are the effective volumetric heat capacity and thermal conductivity of the wet porous medium, calculated as weighted averages of the constituent phases.
The transport fluxes and the evaporation rate are computed using constitutive relations for capillary pressure, relative permeability, and diffusive transport, which are critical for accurately modeling the lithium-ion battery electrode’s drying behavior.
1.3 Coupled Model Setup and Parameters
The geometry for the suspension drying air field is modeled in 2D, representing a cross-sectional slice. This simplification is justified because the electrode’s length and width are orders of magnitude larger than its thickness, and the primary gradients of interest (moisture, temperature) occur across the coating thickness. A schematic of one periodic unit of the nozzle configuration is used for simulation. Key dimensions are summarized in the table below.
| Parameter | Description | Value | Unit |
|---|---|---|---|
| $h$ | Nozzle-to-electrode gap height | 7.5 | mm |
| $\alpha$ | Impingement angle | 45 | ° |
| $w$ | Nozzle slot width | 1.5 | mm |
| $b$ | Spacing between slots | 70 | mm |
| $L$ | Length of periodic domain | 150 | mm |
The boundary conditions for the air field model are as follows: a velocity inlet with specified temperature and turbulence intensity (5%) at the nozzle slots, a pressure outlet at the domain exits, adiabatic walls on the nozzle surfaces, and a moving wall with a constant temperature (approximating the electrode surface) at the bottom. The electrode drying model requires boundary conditions at its top (exposed) and bottom (current collector) surfaces. The bottom is impermeable and adiabatic. The top surface boundary conditions couple the model to the air field results:
$$
\begin{aligned}
\text{Mass Flux:} \quad & n_l + n_v = \varepsilon H_m (\rho_v – \rho_{v,\text{amb}}) \\
\text{Heat Flux:} \quad & \lambda_{\text{eff}} \frac{\partial T}{\partial z} = H_t (T_{\text{amb}} – T) – h_{\text{vap}} n_l \\
\text{Pressure:} \quad & p_g = p_{\text{amb}}
\end{aligned}
$$
Here, $H_m$ and $H_t$ are the convective mass and heat transfer coefficients obtained from the air field simulation, $\rho_{v,\text{amb}}$ is the vapor density in the ambient air, $T_{\text{amb}}$ is the ambient air temperature, and $p_{\text{amb}}$ is atmospheric pressure.
The material properties and model parameters for a typical NMP-based cathode coating are listed below.
| Parameter Group | Parameter | Symbol | Value | Unit |
|---|---|---|---|---|
| Gas Phase (Air/Vapor) | Air Density | $\rho_a$ | 1.205 | kg/m³ |
| Air Dynamic Viscosity | $\mu_a$ | 1.8×10⁻⁵ | Pa·s | |
| Vapor-Air Diffusion Coefficient | $D_{v,a}$ | 2.6×10⁻⁵ | m²/s | |
| Latent Heat of Vaporization (NMP) | $h_{\text{vap}}$ | ~5.4×10⁵ | J/kg | |
| Ambient Relative Humidity | RH | 0.2 | – | |
| Liquid Phase (Solvent) | Liquid Density (NMP) | $\rho_l$ | 824 | kg/m³ |
| Liquid Dynamic Viscosity (NMP) | $\mu_l$ | 4.85×10⁻⁴ | Pa·s | |
| Liquid Absolute Permeability | $K_{a,l}$ | 5×10⁻¹⁴ | m² | |
| Initial Saturation | $S_{l,0}$ | 1.0 | – | |
| Solid Matrix (Electrode) | Porosity | $\varepsilon$ | 0.75 | – |
| Coating Thickness | $h_{\text{coat}}$ | 150 | µm | |
| Solid Density (LFP approx.) | $\rho_s$ | 3600 | kg/m³ | |
| Process Conditions | Base Air Temperature | $T_{\text{amb}}$ | 353.15 – 373.15 | K |
| Base Air Velocity | $v_{\text{in}}$ | 1.1 – 3.6 | m/s | |
| Web Speed | $v_{\text{sub}}$ | 1.0 | m/s |
2. Model Validation
Before employing the model for parametric studies, its predictive capability was rigorously validated against established literature data in two key aspects: the air-side convective transport and the drying kinetics of the porous electrode.
2.1 Validation of the Suspension Drying Air Field Model
The accuracy of the CFD model in predicting the convective environment was tested by reproducing the work on suspension drying nozzle flow fields. The simulated distribution of the local heat transfer coefficient ($H_t$) along the electrode surface was compared with published results. The comparison showed excellent agreement in the profile shape, capturing the characteristic peaks under the impingement zones and the lower values in the recirculation regions. The area-averaged heat transfer coefficient $H_{t,avg}$ was calculated from the simulated convective heat flux $q_{\text{con}}$ and the driving temperature difference:
$$
H_{t,avg} = \frac{q_{\text{con}}}{T_{\text{amb}} – T_0}
$$
For the base case conditions (Re=1000, $T_{\text{amb}}$=373.15 K, $T_0$=293.15 K), the model yielded $H_{t,avg} \approx 43.0 \, \text{W/(m}^2 \cdot \text{K)}$. This value is within 8% of the reference value of 46.8 $\text{W/(m}^2 \cdot \text{K)}$, confirming the model’s reliability in characterizing the convective boundary condition essential for the electrode drying simulation.
2.2 Validation of the Electrode Drying Model
The coupled heat and mass transfer model within the porous electrode was validated by simulating drying curves under two different constant air temperatures (80°C and 100°C) at a fixed air velocity. The simulation results for the drying rate versus moisture content (dry basis) were plotted against experimental data from literature. As shown in the comparative graphs, the model accurately captures the transition from the constant rate period (where drying is limited by external conditions) to the falling rate period (where internal mass transfer becomes dominant). The close match between the simulated and experimental curves under both temperature conditions validates the constitutive relations for capillary flow, vapor diffusion, and evaporation kinetics used in the model. This gives confidence in the model’s ability to predict the drying behavior of a lithium-ion battery electrode under varying process parameters.
3. Results and Discussion: Process Parameter Analysis
Using the validated model, a systematic investigation was conducted to understand how strategic control of drying parameters can enhance drying efficiency and reduce energy consumption in lithium-ion battery electrode manufacturing.
3.1 Influence of Time-Varying Air Temperature Profile
In industrial dryers, air temperature is often not constant but follows a profile along the dryer length (which correlates with drying time). We investigated five distinct temporal temperature profiles, all having the same average temperature of 118°C over a 56-second drying cycle, to isolate the effect of the temperature trajectory. The profiles, defined by piecewise linear equations, are categorized as follows:
| Profile Type | Time Interval (s) | Governing Equation | Description |
|---|---|---|---|
| A: Rise-Then-Fall | 0-32 32-56 |
$T = 109.5 + 0.491t$ $T = 143.1 – 0.536t$ |
Temperature increases linearly, then decreases. |
| B: Fall-Then-Rise | 0-32 32-56 |
$T = 126.6 – 0.560t$ $T = 90.1 + 0.620t$ |
Temperature decreases linearly, then increases. |
| C: High-Then-Low | 0-32 32-56 |
$T = 124$ $T = 112$ |
Constant high temperature, then constant lower temperature. |
| D: Low-Then-High | 0-24 24-56 |
$T = 112$ $T = 124$ |
Constant low temperature, then constant higher temperature. |
| E: Constant | 0-56 | $T = 118$ | Constant average temperature. |
The simulated drying curves revealed significant differences. Profile C (High-Then-Low) consistently achieved the shortest drying time and the highest initial drying rate. The underlying mechanism is physically intuitive: applying a high temperature at the initial stage, when the coating surface is wet, maximizes the convective heat flux. This rapidly supplies the latent heat needed for evaporation, establishing a strong vapor pressure gradient that drives fast solvent removal from the surface and upper layers. Although the temperature is lowered in the later stage, most of the freely available solvent has already been removed, and the process is entering the internal-mass-transfer-limited falling rate period where a slightly lower temperature has a less detrimental effect on the overall timeline. Conversely, Profile D (Low-Then-High) exhibited the slowest drying, as the initial low temperature fails to establish a strong drying impetus.
A critical finding was the relationship between drying time and energy consumption. While the total heat energy supplied by the air per cycle was similar for all profiles (due to the same average temperature), the operational energy consumption is directly tied to the dryer’s active running time. Therefore, a shorter drying time translates into lower fan, pump, and heater runtime costs. The comparative analysis clearly showed that Profile C not only provided the fastest drying but also led to the lowest effective energy consumption, making it the optimal strategy among the tested profiles for the lithium-ion battery electrode drying process.
3.2 Influence of Inlet Air Velocity
The inlet air velocity ($v_{\text{in}}$) is another powerful lever to control the drying process. Simulations were conducted for Profile C (High-Then-Low temperature) at velocities ranging from 1.1 m/s to 3.6 m/s. The results demonstrated a clear trend: increasing air velocity accelerates drying. The drying rate curves showed higher peaks and the total drying time decreased monotonically with velocity. This is because a higher velocity intensifies the convective transfer processes. The heat transfer coefficient $H_t$ increases, delivering more thermal energy to the electrode surface. Simultaneously, the mass transfer coefficient $H_m$ increases, which more efficiently removes the saturated solvent vapor from the surface, maintaining a steeper vapor concentration gradient that is the driving force for evaporation.
However, this performance gain comes at an energy cost. The power required to drive the fans in a drying oven scales approximately with the cube of the air velocity ($P \propto v^3$). Therefore, while drying time ($t_{\text{dry}}$) decreases, the energy consumption per drying cycle ($E_{\text{dry}}$) increases. To identify the most economically efficient operating point, both metrics were analyzed together. The drying time and energy consumption for each velocity were normalized relative to their values at the lowest velocity (1.1 m/s):
$$
t_{\text{norm}} = \frac{t_i}{t_{\text{dry,ref}}}, \quad E_{\text{norm}} = \frac{E_i}{E_{\text{dry,ref}}}
$$
Plotting these normalized values revealed a trade-off curve. The intersection point of the two trends indicates a balance between time efficiency and energy expenditure. For this specific lithium-ion battery electrode and dryer configuration, the optimum was found at an air velocity of approximately 2.0 m/s. At this point, the significant reduction in drying time is not yet offset by the sharply rising energy costs, representing a favorable compromise for minimizing overall production cost per electrode.
4. Conclusions
This study successfully developed and validated a comprehensive CFD-based model to simulate the complex drying process of a lithium-ion battery electrode in a suspension dryer. The model couples the external convective air field with the internal heat and mass transfer within the porous electrode coating. Through detailed numerical experiments, the following key conclusions were drawn for process optimization:
- Time-Varying Temperature Strategy: The profile of the drying air temperature has a profound impact on efficiency. A High-Then-Low temperature profile is highly recommended. It leverages a high initial temperature to maximize the evaporation rate during the critical constant-rate period when the surface is wet, leading to the shortest overall drying time and consequently the lowest operational energy consumption compared to constant or other time-varying profiles with the same mean temperature.
- Optimal Air Velocity: Increasing the inlet air velocity consistently improves the drying rate but at the expense of higher energy consumption due to the cubic relationship between fan power and velocity. An economic optimum exists where the benefit of reduced drying time balances the cost of increased energy use. For the modeled system, this optimum was identified at an air velocity of approximately 2.0 m/s.
These findings provide concrete, model-driven guidance for optimizing the drying stage in lithium-ion battery manufacturing. Implementing a High-Then-Low temperature profile alongside a carefully selected air velocity can significantly enhance production throughput, reduce energy costs, and potentially improve electrode quality by promoting more uniform drying. This work underscores the value of numerical simulation as an indispensable tool for demystifying complex industrial processes and enabling data-informed sustainable manufacturing practices for advanced energy storage devices like the lithium-ion battery.