
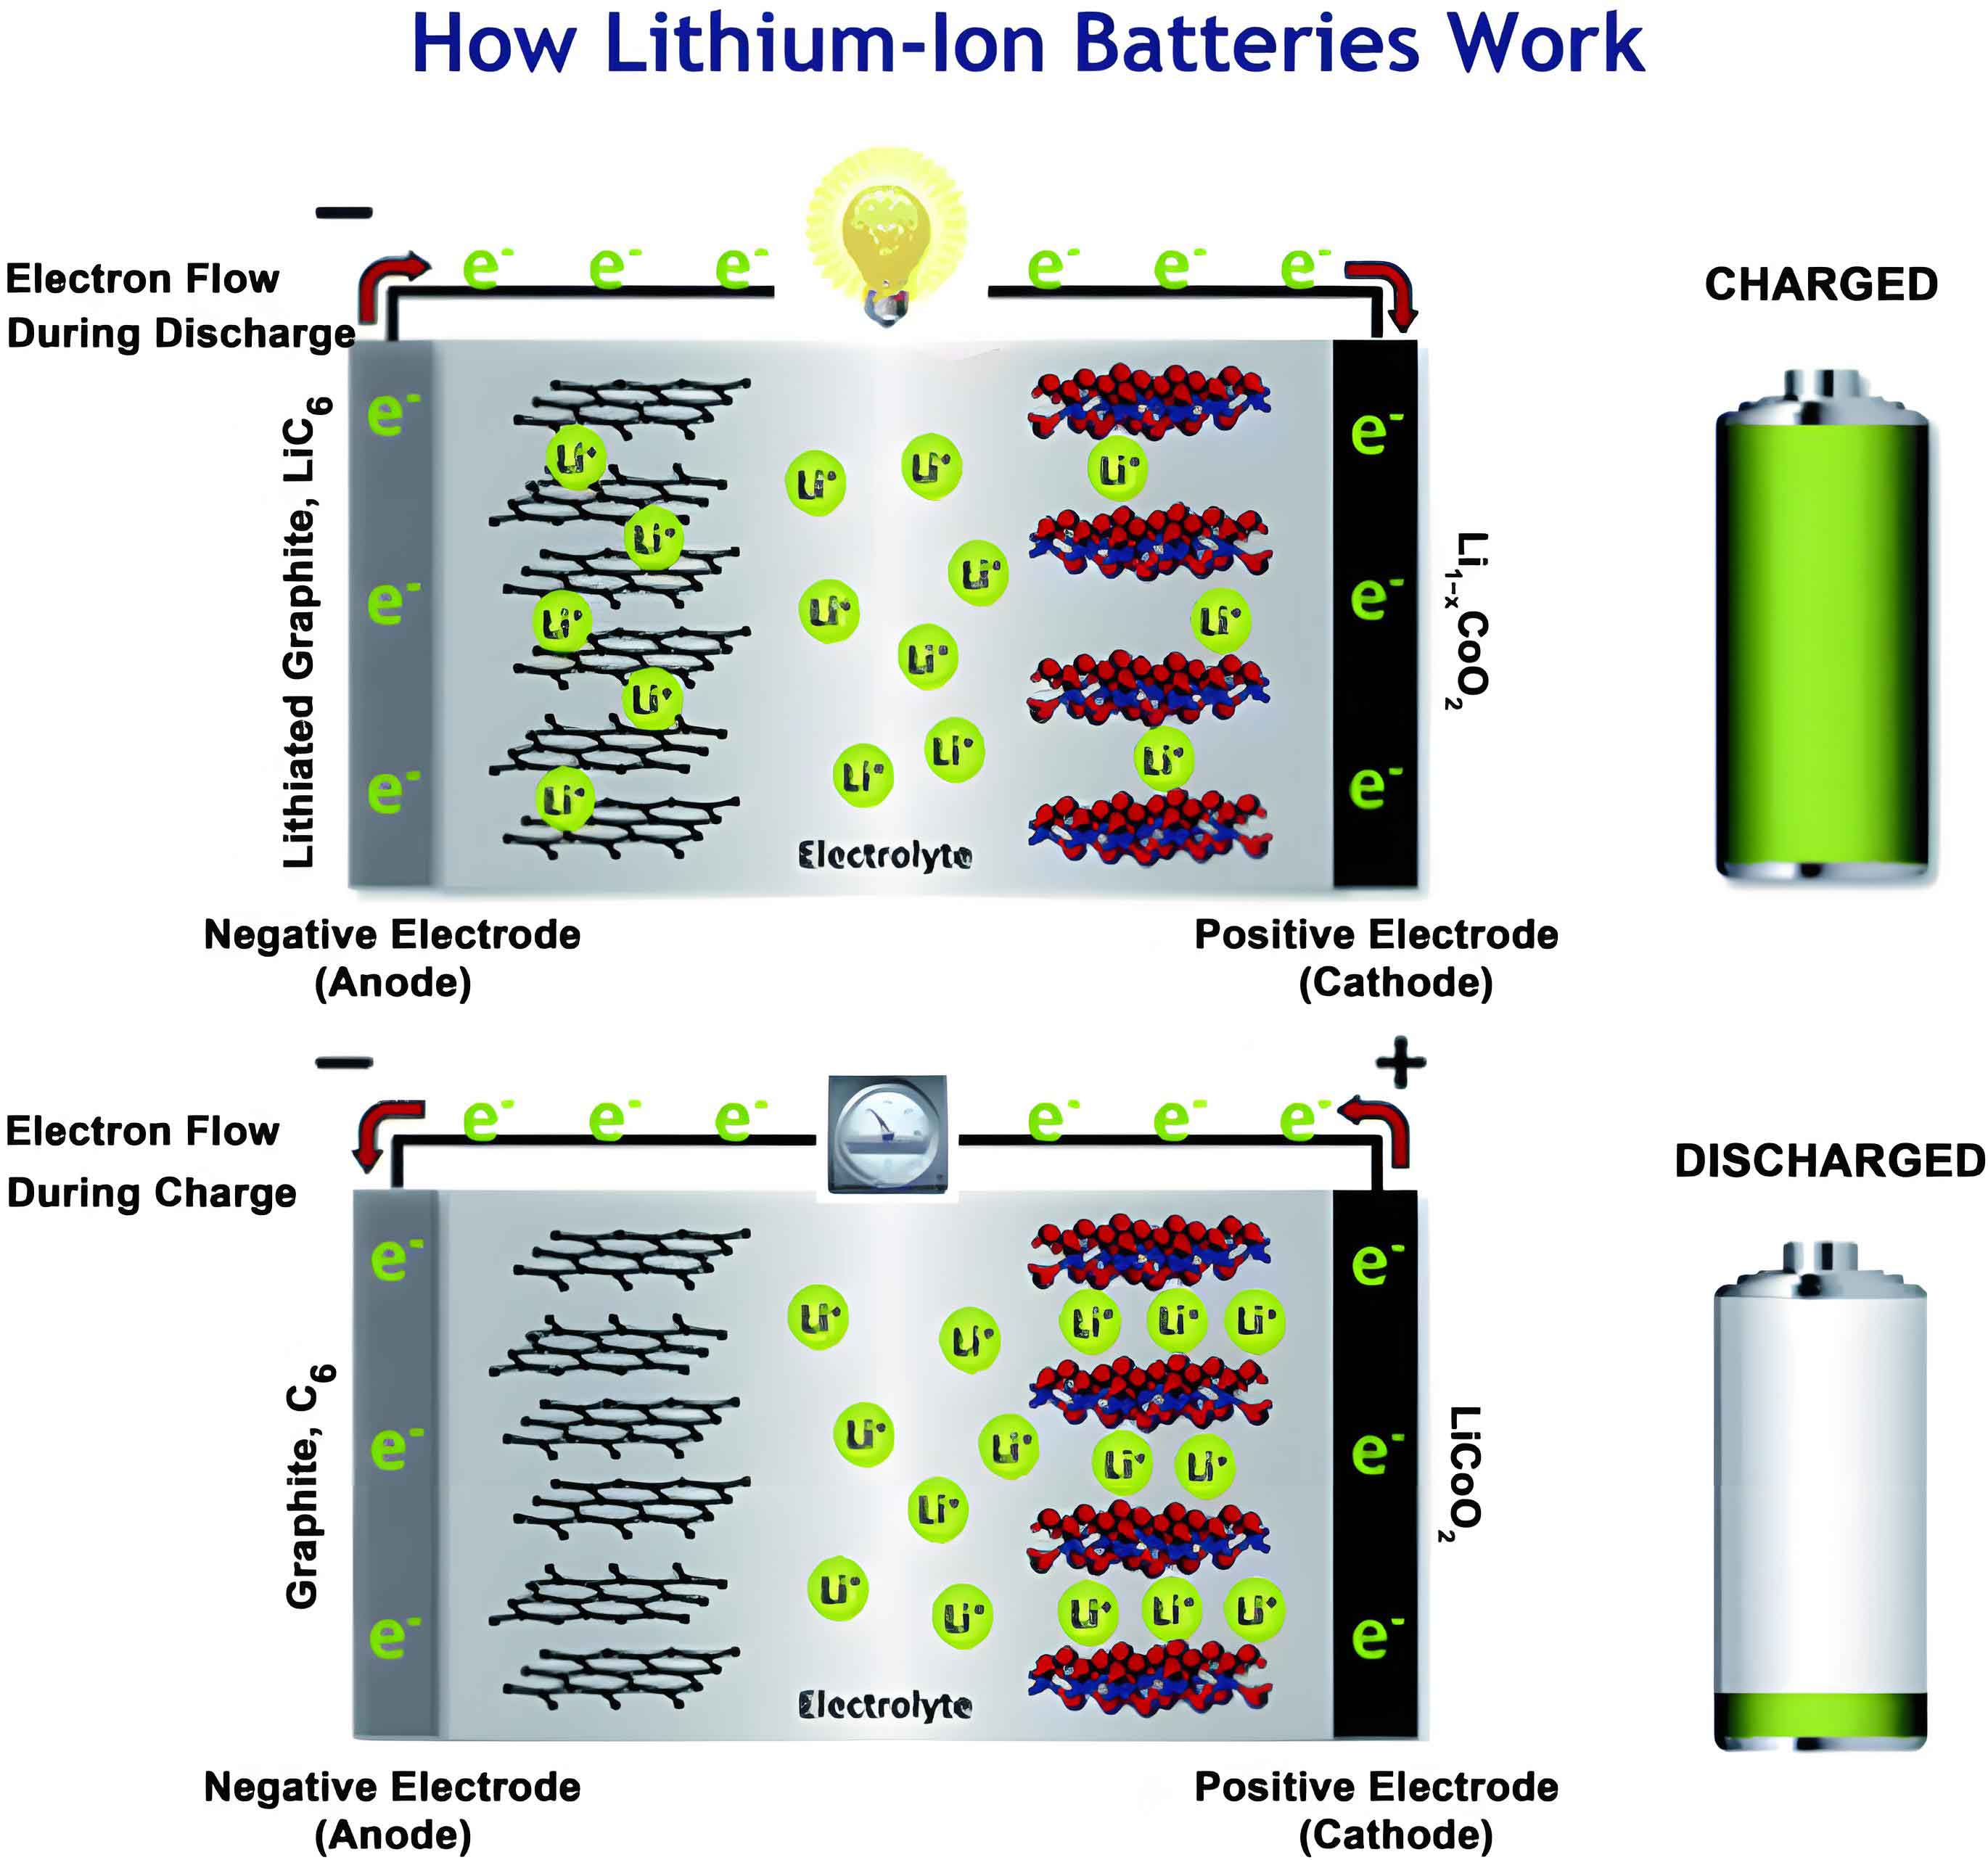
Lithium-ion batteries (LIBs) stand as a cornerstone of modern energy technology, powering everything from electric vehicles and portable electronics to large-scale renewable energy storage systems due to their high energy density and efficiency. Within the complex architecture of a lithium-ion battery, the separator plays a critical yet often understated role. Positioned between the cathode and anode, it must allow for the facile transport of lithium ions while completely blocking electrical contact between the electrodes. The performance of this component directly influences key battery metrics: safety, rate capability, cycle life, and manufacturing yield.
Polypropylene (PP) membranes, produced via a dry process, dominate the commercial market for lithium-ion battery separators owing to their established manufacturing processes and relatively low cost. However, as the industry pushes towards larger-format pouch-type lithium-ion batteries for increased energy capacity, several inherent limitations of PP separators become pronounced. These membranes often exhibit insufficient mechanical strength, leading to risks of deformation in large cells. Their non-polar nature can result in poor wettability by polar carbonate-based electrolytes, and they are prone to thermal shrinkage and wrinkling during processing. Such wrinkles can induce local current hotspots, leading to electrode defects like black spots and even lithium plating, which severely compromise the safety and longevity of the lithium-ion battery.
To overcome these challenges, coating technologies have been widely explored to functionalize separator surfaces. While inorganic coatings like Al2O3 or SiO2 can improve thermal stability, their weak interfacial adhesion with the polymer substrate can lead to delamination. Organic binders like PVDF offer better adhesion but often require energy-intensive thermal lamination processes and involve environmentally concerning fluorinated compounds. In this context, water-based polymethyl methacrylate (PMMA) emerges as a promising alternative. PMMA possesses excellent electrochemical stability, high resistance to electrolyte corrosion, and low swelling. More importantly, specific formulations can be engineered to exhibit remarkable cold-press adhesion properties, enabling strong bonding between the separator and electrodes at room temperature without additional solvents or heat. This presents a significant opportunity to streamline the manufacturing of lithium-ion batteries while enhancing cell integrity.
Our study systematically investigates the impact of a novel PMMA-based adhesive coating on a PP substrate for large-format, 50 Ah stacked pouch lithium-ion batteries. We focus on a comparative analysis between conventional PP separators and our developed PMMA-coated separators, evaluating their influence on both the manufacturing process and the final electrochemical performance of the lithium-ion battery.
1. Materials, Fabrication, and Characterization Methods
1.1 Materials and Electrode Preparation
The cathode was formulated using lithium iron phosphate (LiFePO4) as the active material, mixed with conductive graphite and PVDF binder in a weight ratio of 96:1.5:2.5. N-Methyl-2-pyrrolidone (NMP) served as the solvent. The anode consisted of graphite as the primary active material, with conductive graphite, polyacrylic acid (PAA) binder, and sodium carboxymethyl cellulose (CMC) dispersant in a weight ratio of 96.5:0.5:2.5:0.5, using deionized water as the solvent. The slurries were coated onto 12 μm aluminum foil (cathode) and 4.5 μm copper foil (anode), respectively, followed by drying, calendering, and slitting to create the final electrode sheets.
The baseline separator was a commercially available 16 μm thick dry-process PP membrane. The experimental separator was a 14 μm thick PP base membrane coated symmetrically on both sides with a functional PMMA-based adhesive layer, with each side’s coating being approximately 1 μm thick. The areal density of the coating was controlled between 0.7-1.3 g/m². The adhesive was designed as a core-shell latex particle. The core, composed of relatively rigid PMMA, provided mechanical integrity. The shell, made from polyacrylate with a designed glass transition temperature (Tg) of -45°C to -35°C, ensured excellent cold-press adhesion at room temperature. Furthermore, the shell was grafted with polar functional groups (e.g., carboxyl, hydroxyl) to enhance electrolyte affinity and lithium-ion transport kinetics. The electrolyte used was a 1.0 M LiPF6 solution in a mixture of ethylene carbonate (EC), ethyl methyl carbonate (EMC), and dimethyl carbonate (DMC).
1.2 Separator and Battery Characterization
The physical properties of the separators, including thickness, air permeability (Gurley value), puncture strength, tensile strength, and thermal shrinkage, were measured according to the national standard GB/T 36363-2018. Electrolyte wettability was assessed by the contact angle using a sessile drop method. The electrolyte uptake (ρ) was determined gravimetrically. A separator sample was dried at 70°C for 12 hours and weighed (W0). It was then immersed in the electrolyte for 6 hours, wiped gently to remove surface liquid, and weighed again (Wt). The uptake was calculated as:
$$ρ = \frac{W_t – W_0}{W_0} \times 100\%$$
The ionic conductivity (σ) of the separator saturated with electrolyte was evaluated using electrochemical impedance spectroscopy (EIS). A symmetric stainless steel (SS) | separator | SS cell was assembled. After resting for 12 hours, EIS was performed with an amplitude of 10 mV over a frequency range from 1 MHz to 0.1 Hz. The bulk resistance (Rb) was obtained from the high-frequency intercept on the real axis. The ionic conductivity was calculated using the formula:
$$σ = \frac{l}{R_b \times A}$$
where \(l\) is the thickness of the separator (in cm) and \(A\) is the contact area of the electrode (in cm²).
1.3 Battery Assembly and Electrochemical Testing
The 50 Ah pouch lithium-ion batteries were assembled using a standardized stacking process. Two cell designs were prepared for comparison: Scheme A (Control) using the conventional PP separator, and Scheme B (Experimental) using the PMMA-coated separator. Key cell design parameters are summarized in Table 1. After stacking, the jellyrolls underwent a cold-pressing process. For the PMMA-coated separator group, an optimized pressure of 8 MPa was applied for 4 seconds to activate the adhesive property. The cells were then dried, filled with a controlled amount of electrolyte (168 ± 2 g), sealed, and formed.
All electrochemical tests were performed using a high-precision battery test system. The formation protocol involved charging at 0.033C to 3.65V. The standard capacity was determined by charging at 0.33C to 3.65V (constant current, CC) and then holding at 3.65V (constant voltage, CV) until the current dropped to 0.025C, followed by a 1.0C discharge to 2.5V. The average of the first three cycles was taken as the nominal capacity. Rate capability tests involved CC-CV charging at various rates (0.33C, 0.5C, 1.0C) and CC discharging at various rates (0.5C, 1.0C, 1.5C). High-temperature (55°C) and low-temperature (-10°C) discharge tests were conducted after full charging at 25°C. Cycle life tests were performed at 25°C and 55°C using a 0.5C charge / 1.0C discharge protocol.
| Parameter | Value |
|---|---|
| Cathode Active Material | LiFePO4 |
| Anode Active Material | Graphite |
| Cell Capacity (Design) | 50 Ah |
| Cell Dimensions (L × W) | 252 mm × 161 mm |
| Cathode Loading | 380 g/m² |
| Anode Loading | 171 g/m² |
| N/P Ratio | 1.15 |
| Electrolyte Amount | 168 ± 2 g |
2. Results and Discussion
2.1 Characterization of the PMMA Coated Separator
The surface morphology of the separators was examined by scanning electron microscopy (SEM). The bare PP separator exhibited a smooth surface with a characteristic microporous network structure resulting from the dry-stretching process. In contrast, the PMMA-coated separator showed a uniform layer of adhesive particles covering the surface. The underlying porous structure of the PP substrate remained accessible, indicating that the coating did not completely block the ion-transport pathways but rather functionalized the surface.
A comprehensive comparison of physical properties is presented in Table 2. While the overall thickness was maintained at 16 μm, the coated separator showed a slight increase in Gurley value (from 240 to 262 s/100 mL), confirming a partial filling of pores but within an acceptable range for a lithium-ion battery. The most significant improvements were in surface properties and mechanical integrity. The contact angle with electrolyte dropped dramatically from 54.4° to 37.4°, indicating superb wettability. Consequently, the electrolyte uptake (ρ) increased by over 130%, from 339.4% to 808.5%. This enhanced wettability and retention directly contributed to a substantial increase in ionic conductivity (σ), which surged from 2.92 × 10⁻⁴ S/cm to 10.73 × 10⁻⁴ S/cm.
Mechanically, the puncture strength improved by over 50%, and the machine direction (MD) tensile strength increased significantly. These enhancements suggest the PMMA coating forms a reinforcing composite structure with the base film. Crucially for safety and processing, the thermal shrinkage was drastically reduced. After 12 hours at 90°C, the MD shrinkage of the coated separator was only 0.8%, compared to 3.0% for the bare PP separator. This superior thermal stability is attributed to the higher thermal decomposition temperature of PMMA and the restraining effect of the coating layer, which is vital for preventing internal short circuits in a lithium-ion battery under abuse conditions.
| Property | PP Separator | PMMA Coated Separator |
|---|---|---|
| Thickness (μm) | 16 | 16 |
| Gurley Value (s/100 mL) | 240 | 262 |
| Contact Angle (°) | 54.4 | 37.4 |
| Electrolyte Uptake, ρ (%) | 339.4 | 808.5 |
| Ionic Conductivity, σ (10-4 S/cm) | 2.92 | 10.73 |
| Puncture Strength (gf) | 221 | 337 |
| MD Tensile Strength (kgf/cm²) | 1650 | 2011 |
| TD Tensile Strength (kgf/cm²) | 150 | 154 |
| MD Thermal Shrinkage @90°C/12h (%) | 3.0 | 0.8 |
| MD Thermal Shrinkage @130°C/0.5h (%) | 3.5 | 1.0 |
2.2 Impact on Lithium-ion Battery Manufacturing Process
2.2.1 Jellyroll Integrity and Short-Circuit Rate
The cold-pressing process was critical for activating the adhesive property of the PMMA coating. We investigated the effect of pressure on jellyroll mechanical strength. Without pressure or at low pressure (4 MPa), the jellyroll remained bendable or lacked flatness. At the optimized condition of 8 MPa for 4 seconds, the jellyroll achieved excellent mechanical rigidity and flatness. The adhesion between the separator and electrodes was strong enough to allow the dry jellyroll to be handled without delamination. This improved structural integrity directly benefited downstream manufacturing. For instance, during the pouch bag loading step prior to sealing, the rigid jellyroll of Scheme B had a much more secure vacuum pickup by the robot compared to the relatively floppy jellyroll of Scheme A, improving process reliability.
This enhanced integrity had a profound effect on cell yield. As shown in Table 3, the incidence of internal short circuits, typically caused by misalignment or intrusion of electrode tabs during ultrasonic welding, was drastically reduced. The welding short-circuit rate dropped from 5.37% for PP-based cells to a mere 0.02% for cells with the PMMA-coated separator. Furthermore, the final packaging short-circuit rate was reduced from 0.49% to 0%. This dramatic improvement in yield is a major economic and quality advantage for manufacturing large-format pouch lithium-ion batteries.
| Defect Type | Scheme A (PP Separator) | Scheme B (PMMA Coated Separator) |
|---|---|---|
| Welding Short-Circuit Rate | 5.37% | 0.02% |
| Final Packaging Short-Circuit Rate | 0.49% | 0.00% |
2.2.2 Cell Appearance and Electrode Interface
Visual inspection of uncycled cells revealed clear differences. Cells from Scheme A often exhibited local deformation and visible separator wrinkle marks on the pouch surface. This is attributed to the weak interfacial adhesion and lower mechanical strength of the jellyroll, allowing it to deform under its own weight or minor external stress. In contrast, cells from Scheme B possessed a perfectly flat and smooth appearance, with no wrinkles, conforming precisely to the intended dimensions. The cold-pressed jellyroll with the adhesive separator acted as a unified, robust structure.
Post-mortem analysis of fully charged cells further highlighted the interface quality. For Scheme A cells, areas corresponding to surface wrinkles often revealed “black spots” on the anode surface, indicative of local degradation or plating due to poor contact and uneven current distribution. The separator itself could show permanent creases. For Scheme B cells, the electrode interfaces were pristine and uniform, with the separator tightly bonded to both electrodes. This intimate contact ensured homogeneous current distribution and mitigated localized Li+ flux, which is essential for preventing lithium plating and ensuring the long-term health of the lithium-ion battery.
2.3 Impact on Electrochemical Performance of the Lithium-ion Battery
2.3.1 Capacity and Storage Performance
The electrochemical performance data is summarized in Table 4. Cells built with the PMMA-coated separator (Scheme B) exhibited a consistently higher baseline capacity compared to those with the PP separator (Scheme A). The average capacity increased by approximately 1.35 Ah, or about 2.5% relative to the Scheme A baseline. This improvement is linked to the superior electrolyte wettability and uptake of the coated separator. During the formation process, better and more uniform wetting promotes the formation of a more effective and stable solid electrolyte interphase (SEI) on the anode, reducing irreversible lithium loss and thereby increasing the active lithium inventory available for cycling in the lithium-ion battery.
Accordingly, the high-temperature (55°C) discharge capacity also showed an improvement of 1-2% for Scheme B. The enhanced electrolyte retention likely provided better ionic transport at elevated temperatures. Low-temperature (-10°C) performance and room-temperature storage showed comparable results between the two schemes.
2.3.2 Rate Capability and Polarization
Rate performance tests provided clear evidence of the benefits of the PMMA coating. At higher charge rates, the constant current (CC) ratio, which indicates the fraction of capacity charged before reaching the voltage limit, was higher for Scheme B. For example, at a 1.0C charge rate, the CC ratio for Scheme B was about 0.6% higher than for Scheme A. This indicates lower polarization during charging. Similarly, during discharge, Scheme B cells retained more capacity at high rates (1.0C and 1.5C), with discharge capacity ratios approximately 1% higher.
The discharge voltage profiles visually demonstrate this reduced polarization. At equivalent states of discharge, the operating voltage of Scheme B cells was consistently higher than that of Scheme A cells during discharge (and lower during charge), indicating a lower overall cell impedance. This can be attributed to multiple factors: 1) The higher ionic conductivity (σ) of the separator system, 2) The reduced interfacial resistance due to excellent electrode-separator adhesion and contact, and 3) The potential gelling effect of the PMMA with the electrolyte, which may create more continuous ion-conduction pathways. These factors collectively enhance the power capability of the lithium-ion battery.
2.3.3 Cycle Life Performance
The long-term cycling stability is a critical metric for any lithium-ion battery. Figure 1 illustrates the cycle life comparison. At 25°C, both cell types showed an initial capacity rise due to the typical activation process of LiFePO4. However, after 500 cycles, the capacity retention of Scheme B cells was approximately 5 percentage points higher than that of Scheme A cells. The improvement was also evident under more stressful 55°C cycling conditions, where Scheme B exhibited about 3.2% higher capacity retention after 500 cycles.
The mechanism behind the improved cycle life is multifaceted. The strong adhesive bond maintains intimate interfacial contact throughout the repeated expansion and contraction of the graphite anode during cycling. This prevents delamination and the associated increase in local impedance. Furthermore, the stable and uniform SEI formed initially is less prone to cracking and reformation, reducing continuous electrolyte decomposition and active lithium consumption. The coating itself may also act as a mechanical buffer, absorbing some of the strain from electrode volume changes, thereby contributing to the structural stability of the entire lithium-ion battery during long-term operation.
| Test Item | Scheme A (PP) | Scheme B (PMMA Coated) |
|---|---|---|
| Average Baseline Capacity (Ah) | 51.8 | 52.5 |
| 55°C Discharge Capacity Ratio (%) | ~101.4 | ~102.6 |
| 1.0C Charge CC Ratio (%) | ~97.2 | ~97.8 |
| 1.5C Discharge Capacity Ratio (%) | ~96.5 | ~97.4 |
| Capacity Retention @25°C / 500 cycles | Lower | ~5% higher |
| Capacity Retention @55°C / 500 cycles | Lower | ~3.2% higher |
3. Conclusion
Our comprehensive study demonstrates that the application of a functional PMMA-based adhesive coating onto a conventional PP separator delivers significant multifunctional benefits for large-format pouch lithium-ion batteries. The coating strategy successfully addresses several key limitations of standard separators.
Firstly, the PMMA coating substantially improves the physical and interfacial properties: it enhances electrolyte wettability (contact angle reduced from 54.4° to 37.4°), boosts electrolyte uptake by over 130%, increases ionic conductivity by a factor of ~3.5, and improves mechanical and thermal stability. These intrinsic material improvements lay the foundation for enhanced battery performance.
Secondly, and critically for manufacturing, the cold-press adhesive property of the coating revolutionizes the cell assembly process. It transforms the jellyroll into a mechanically robust, unified structure. This leads to a dramatic reduction in manufacturing defects, with short-circuit rates during welding and packaging dropping from 5.37% and 0.49% to 0.02% and 0%, respectively. The resulting lithium-ion battery cells exhibit excellent dimensional accuracy and a pristine, wrinkle-free appearance.
Finally, these processing and material advantages translate directly into superior electrochemical performance. The lithium-ion batteries employing the PMMA-coated separator show higher baseline capacity (~2.5% increase), improved rate capability (e.g., ~1% higher capacity at 1.5C discharge), and significantly extended cycle life (e.g., ~5% higher capacity retention after 500 cycles at 25°C). The mechanisms are attributed to better SEI formation, reduced interfacial resistance, maintained electrode contact, and lower overall cell polarization.
In conclusion, this PMMA-coated separator technology presents a highly effective and industrially viable solution to enhance the manufacturability, yield, safety, and performance of next-generation large-format pouch lithium-ion batteries. It represents a significant step forward in separator design, moving from a passive component to an active, multi-functional element that integrates seamlessly into advanced lithium-ion battery systems.